Urethane Concrete · Industrial Epoxy · ESD · Hangar Floor Coatings
The Toughest Industrial Floors Built to Last 20+ Years
30+ yrs
Direct Manufacturer Experience
20+ yrs
Typical Floor Service Life
50 states
Certified Contractors & Installers
5-yr
Written Material & Workmanship Warranty
About PumaCRETE
PumaCRETE manufactures high-performance urethane concrete flooring, polyurethane cement mortar, industrial epoxy floor coatings, ESD and anti-static systems, conductive epoxy flooring, antimicrobial sanitary flooring for food plants, and Skydrol-resistant aircraft hangar coatings, all engineered to outlast the building. Installation is performed by our nationwide network of factory-certified independent contractors. Our ANSI/ESD S20.20-compliant static-dissipative ESD flooring serves clean rooms, data centers, and robotics environments. For defense and military facilities, PumaCRETE supplies DoDM 4145.26-compliant conductive flooring for ammunition, explosives, and ordnance handling. We also provide hangar and MRO flooring with MIL-PRF-compatible chemistry that stands up to Skydrol, jet fuel, de-icing fluids, and heavy aircraft and ground-support equipment loads.
Our systems serve armories, munitions plants and magazines, avionics and electronics repair shops, motor pools and vehicle maintenance bays, battery rooms, command and data centers, and military dining and galley facilities. Our food-grade systems are USDA-acceptable, FDA-compliant, and SQF and HACCP audit-ready. Our cementitious urethane systems survive hot wash-downs, caustic CIP, organic acids, antimicrobial cleaning chemistry, dropped tooling, and 24/7 forklift traffic. PumaCRETE has over a decade as a direct manufacturer, backed by a nationwide network of factory-certified installers and a 5-year written warranty on material and workmanship.
Industrial Floor Coatings Trusted Where Failure Isn't an Option
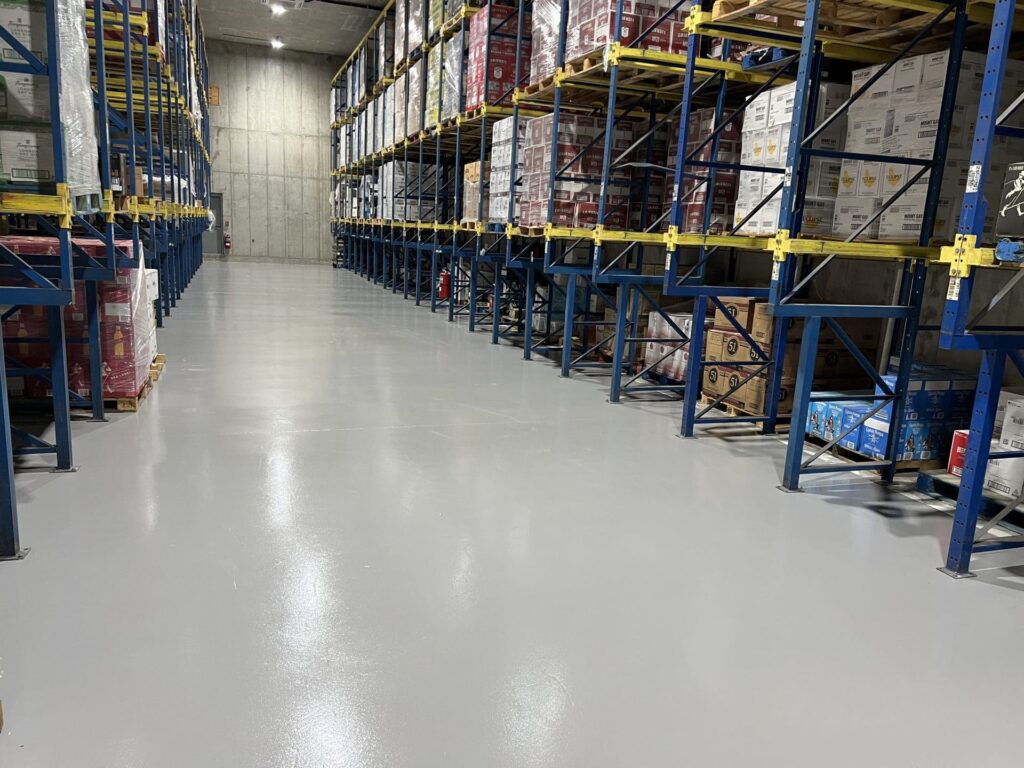
For three decades, PumaCRETE industrial floor coatings, urethane concrete flooring, ESD flooring, and aircraft hangar floor coatings have been specified in the facilities where downtime costs millions, audits are non-negotiable, and the floor has to last as long as the building. From USDA-FSIS food plant floor installations to ANSI/ESD S20.20 cleanroom epoxy floor systems to MIL-PRF aircraft hangar epoxy flooring — every system is engineered for the exact failure mode it has to survive.
Urethane concrete, polyurethane cement, and epoxy systems for warehouse, manufacturing, factory, and distribution facilities. Chemical-resistant and non-slip options across every traffic load. Industrial Flooring →
USDA-approved sanitary urethane concrete for meat, seafood, dairy, bakery, brewery, distillery, winery, and produce processing facilities. Antimicrobial topcoat options available. Food Plant Flooring →
ANSI/ESD S20.20-compliant static-dissipative and conductive systems for electronics, cleanrooms, data centers, AGV and Robot pathways, and munitions storage. ESD Flooring →
Skydrol-, jet-fuel-, and hydraulic-fluid-resistant epoxy and polyaspartic systems for military, MRO, and FBO hangars. DOD 4145.26-M aligned chemistry. Hangar Flooring →
Every Floor Category We Offer
Industrial Flooring Solutions Across Every Sector We Serve
PumaCRETE manufactures a different chemistry, thickness, and finish for each industry. Find the dedicated page for your facility type.
Manufacturing & Warehouse Floors
Food & Beverage Processing
Brewery Flooring
Distillery Flooring
Dairy Plant Flooring
Bakery Flooring
Seafood Processing
Beef, Pork & Poultry Plants
ESD & Conductive Floors
Cleanroom & Electronics
Data Center Anti-Static
AGV & Robot Areas
Munitions & AA&E
Aircraft Hangars
USPS Workrooms (401-ECO)
Caribbean Food Plants
Urethane Concrete Cost Guide
Compare to Ucrete & Stonhard
The PumaCRETE Product Line
Five Product Families — One Specification, Built for Your Plant
PumaCRETE manufactures a full range of resinous flooring chemistries — from thin-mil industrial epoxy floor coatings to half-inch troweled urethane concrete to ANSI/ESD S20.20-compliant ESD floor coatings.
| Series | Thickness | Best For | Finish |
|---|---|---|---|
| PumaCRETE 100 / 200 Series | 12–60 mils (0.012–0.060 in.) | Industrial epoxy floor coating, warehouse floor, light-medium duty, clean room flooring | Roll-applied coating, satin to gloss |
| PumaCRETE 300 Series | 1/16 to 1/4 inch | Heavy-duty industrial flooring, food packaging, wet/damp areas, industrial floor repair | Trowel-textured, broadcast aggregate |
| PumaCRETE 400 / 401-HF Series | 1/4 to 3/4 inch | Urethane concrete flooring — food plant floor, brewery, dairy, meat, seafood, severe service | Trowel-applied urethane mortar |
| PumaCRETE 401-ECO | 1/4 to 1/2 inch | USPS workrooms, government, federal projects with fast turnaround | Trowel-applied screed, low-odor, fast cure |
| Puma-ESD Series | 12 mils to 1/4 inch | ESD flooring, antistatic flooring, conductive flooring — electronics, AGV, data center, munitions | Satin to semi-gloss, ANSI/ESD S20.20 |
ESD Flooring & Static-Control Floor Coatings
ANSI/ESD S20.20-Compliant ESD Flooring for Static-Sensitive Facilities
PumaCRETE Puma-ESD systems control electrostatic discharge in the facilities where it costs money or threatens safety. Every system is independently tested against ANSI/ESD S20.20 for surface-to-ground resistance and body-voltage generation, and installed by factory-certified ESD floor installers who provide documented test results at project handover.
Static-Dissipative Systems (10⁶–10⁹ Ω)
Specified for electronics manufacturing, semiconductor cleanrooms, PCB assembly, AGV and Robot corridors, and data centers. Dissipative resistance safely drains static charge while remaining low-conductive enough to satisfy electrical safety codes. Available as a 12-mil epoxy coating, 1/8-inch self-leveling system, or 1/4-inch troweled urethane concrete depending on traffic load.
Conductive Systems (Under 10⁶ Ω)
Engineered for munitions storage, Arms-Ammunition-Explosives (AA&E) rooms, operating theaters, and high-charge-dissipation environments where static discharge is a life-safety hazard. Conductive copper grounding strips are bonded into the substrate before topping pour. Documentation provided for DOD and DOE compliance audits.
Cleanroom & Electronics Manufacturing
Anti-static cleanroom flooring for ISO Class 5 through Class 8 environments. Compatible with ULPA filtration and rated for low particulate emission. Smooth, easy-clean topcoat finish suitable for pharmaceutical, biotech, electronics, and aerospace assembly. Available in both static-dissipative and conductive resistance ranges.
AGV & Robot Pathways
Designed for automated guided vehicle and Robot navigation environments. Sub-3-mm flatness tolerance protects laser-navigation accuracy and wheel-bearing service life. Optional ESD properties prevent charge accumulation on vehicle frames and chassis. Used in fulfillment centers, automotive assembly, and high-throughput logistics.
Data Center Anti-Static Floors
Anti-static epoxy floor coatings for server halls, network operations centers, and switching rooms. Protects sensitive IT infrastructure from electrostatic damage during maintenance and equipment moves. NFPA-99 compatible. Light-reflective topcoats improve visibility in dim equipment aisles.
Munitions & Explosive Atmosphere Areas
Conductive flooring meeting NFPA 484 and DOD 4145.26-M requirements for facilities handling Class 1 Division 1 explosive atmospheres. Used in munitions production, propellant handling, ordnance assembly, and pyrotechnics. Independent surface-resistance certification provided at installation.
Food & Beverage Processing Flooring
USDA-Approved Urethane Concrete for Food Plant Flooring
PumaCRETE urethane concrete meets the seamless-resinous-flooring requirements of USDA 9 CFR Part 416 and the FDA Food Code, and supports SQF, BRC, IFS, FSSC 22000, and HACCP audit programs. The cementitious urethane chemistry resists organic acids, hot wash-downs, caustic CIP cleaning, and the thermal cycling that destroys ordinary epoxy floors in operating food and beverage plants. Service and documentation are also available in Spanish for Caribbean and Latin American facilities.
Meat & Poultry Processing
Engineered for USDA-FSIS inspected facilities — kill floors, evisceration, cut rooms, chillers, packaging, and shipping docks. The 400-series urethane concrete withstands constant blood, fat, and organic-acid exposure plus the daily hot-water sanitation cycles that delaminate ordinary epoxy. Available with integral slope-to-drain detailing and stainless cove base.
Seafood & IQF Freezer Floors
Salt brine, fish oil, and ammonia chiller exposure require a fundamentally different chemistry than dry-process flooring. The system installs in operating coolers down to 35°F and resists the thermal-shock cycling typical of IQF freezer-to-thaw operations. Used in fillet lines, smokehouses, and packaging rooms across the seafood industry.
Dairy & Cheese Plants
Lactic acid generated during cheese production destroys most floor systems within a few years. PumaCRETE urethane concrete resists lactic acid at process concentrations and remains compliant with USDA, FDA, and Grade A Pasteurized Milk Ordinance requirements. Used in raw-milk receiving, pasteurization, cheese caves, yogurt rooms, and butter production.
Bakery & Confectionery
Two failure modes destroy bakery floors: sugar attack from spilled product penetrating concrete and oven-heat radiating through the slab. The trowel-applied urethane concrete forms a sealed sugar-impermeable layer and tolerates substrate temperatures well above the limits of conventional epoxy in oven and proofing areas.
Brewery, Distillery & Winery
Hot wort, ethanol, tartaric acid, caustic CIP, and constant wet-floor conditions all attack ordinary epoxy. The system handles brewhouse pad, fermentation cellar, bottling line, and barrel-room service with integrated stainless slot-drain detailing and a slip-resistant texture rated for wet boot traffic.
Produce & Beverage Processing
Engineered for high-volume produce washing, juice and beverage filling lines, and CIP-intensive bottling rooms. Antimicrobial topcoat options are available where biological hygiene control is required, with documented test data for SQF and BRC inspector review.
USDA, FDA & Audit Documentation
Every installation ships with the documentation package your QA team needs: independent test certificates, declaration of conformity to 9 CFR 416, FDA 21 CFR 175.300 indirect-contact compliance letter, and SQF/BRC/IFS audit support documentation. We're regularly cited by name in audit reports.
Antimicrobial Topcoat Options
Silver-ion and zinc-pyrithione antimicrobial additives are available for high-risk hygiene zones. The additive is integral to the topcoat, not a surface treatment, so it remains effective through wear and cleaning. Independent ASTM E2180 and JIS Z 2801 testing data is provided on request.
Spanish-Language Project Support
For Caribbean, Mexican, and Central and South American food processing plants, project management, technical specs, and on-site training are delivered in Spanish. The same urethane concrete chemistry and USDA documentation supports plant audits across the region. Shipping is consolidated through the Port of Miami.
Aerospace & Aircraft Hangar Floor Coatings
Aircraft Hangar Flooring
PumaCRETE aircraft hangar floor coatings are specified for U.S. military hangars, MRO bays, FBO facilities, helipads, and commercial aerospace assembly plants. The high-build epoxy and polyaspartic chemistries are formulated specifically for the chemical exposure that destroys ordinary floors in operational hangars — and qualified against the MIL-PRF specification family required for federal contracting.
Skydrol & Hydraulic Fluid Resistance
Phosphate-ester-based Skydrol attacks ordinary epoxy hangar floor coatings within months. The PumaCRETE chemistry is formulated specifically to resist Skydrol, MIL-PRF-83282, and MIL-PRF-87257 hydraulic fluids. The difference between this and a generic epoxy is the difference between a 5-year and 20-year service life on an operational hangar floor.
Jet Fuel & De-Icing Chemistry
Resists Jet-A, JP-5, JP-8, ethylene glycol de-icing fluid, and propylene glycol Type I-IV deicing chemistry. The surface stays sealed against the repeated chemical exposure typical of operational ramps, aircraft pads, and de-icing pad transitions. Used on flightline and tarmac applications as well as hangar interiors.
Military & DOD 4145.26-M
System chemistry aligned with DOD 4145.26-M and qualified against MIL-PRF-85285 Type IV polyurethane and MIL-PRF-23377 epoxy primer standards. Deployed on B-1, B-52, C-5, C-17, F-15, F-22, F-35, and commercial widebody hangar floors. Buy American Act compatible. Available in DLA QuickSearch for federal contracting.
Light-Reflective Topcoats
High-gloss white and gray topcoats deliver up to 85% light reflectance, meeting MILCON and Unified Facilities Criteria photometric requirements for hangar interior lighting. Improves nighttime visibility on the floor and reduces required lumen output from hangar lighting systems by 20-30%.
Hangar Resurfacing & MRO Renovations
Sound substrates can be resurfaced without full demolition. The 300-series urethane concrete bonds to mechanically prepared concrete in a single trowel pass. Used in California-based MRO operations, FBO renovation projects, and active Air Force hangars where the floor cannot be out of service for more than 72 hours per zone.
Project Cost & Documentation
Typical installed cost ranges from $10 to $18 per square foot depending on substrate condition, system thickness, and topcoat selection. Every quote includes the documentation package federal contracting officers require — material data sheets, test certificates, and specification cross-reference. Factory-certified hangar contractor network nationwide.
Industrial Floor Coatings & Manufacturing Plant Flooring
Industrial Flooring Systems Engineered for Heavy-Duty Service
For manufacturing plants, warehouses, distribution centers, and factories, PumaCRETE manufactures resin chemistries matched to the specific failure mode each environment imposes — forklift impact, thermal cycling, aggressive chemistry, dropped tooling, or 24/7 production loading. Most facilities use a combination of two or three system types across different zones.
Urethane & Polyurethane Cement
For wet processing, hot wash-down, and aggressive chemical exposure. The cementitious urethane chemistry resists thermal shock from -40°F to 248°F, organic and inorganic acids, and the moisture levels that delaminate ordinary epoxy floors. Standard at 1/4 to 3/8 inch thickness.
Industrial Epoxy Systems
For dry-process manufacturing, warehouse, and assembly environments where chemical exposure is moderate and aesthetics matter. Available from 12-mil roll-applied coatings for budget-conscious projects up to 60-mil broadcast systems with decorative quartz finish for showroom-grade industrial spaces.
Polyaspartic Topcoats
For projects requiring fast return to service. Cures in 2-4 hours per coat versus 12-24 for ordinary epoxy. Used in retrofits where the facility cannot be out of service for more than a single shift, and as a UV-stable topcoat over urethane concrete in interior-exterior transition zones.
Floor Repair & Resurfacing
Sound concrete substrates can be resurfaced without full demolition. The 300-series system bonds to mechanically prepared concrete in a single trowel pass, restoring failed epoxy floors and damaged slabs at roughly half the cost of full demolition and replacement.
Chemical-Resistant Specifications
For chemical processing, pharmaceutical manufacturing, plating, and battery production, the system handles concentrated sulfuric, hydrochloric, nitric, and phosphoric acids; sodium and potassium hydroxide; common solvents; and oxidizing chemistries. Specification-grade chemical resistance testing data is provided per ASTM C267 and C868.
Safety & Non-Slip Texture
Permanent integral aggregate is part of the urethane mortar, not a surface broadcast. The slip texture is maintained through the full thickness of the floor, so traction doesn't wear off as the floor sees forklift and foot traffic. OSHA 1910.22 compliant. Coefficient of friction is tunable from 0.6 to 0.9.
Certified Installer Network — Nationwide
Find a Factory-Certified Industrial Flooring Contractor Near You
PumaCRETE operates a network of factory-certified installation crews across all 50 U.S. states. Every crew is trained directly on PumaCRETE chemistry, equipped with diamond grinders, shot blasters, and HEPA dust extraction, and backed by the manufacturer warranty. We match facilities to the right crew based on project scope, sector experience, and certification depth — not whoever bids lowest on RFP day.
Operating-Plant Installation Phasing
Most certified-network installations happen in plants that cannot shut down. Crews are experienced at zoning, dust containment, food-safe staging, and weekend shutdown sequencing. For food and pharmaceutical facilities, the installation team coordinates directly with your QA group on sanitation cycles before and after each phase.
DIY Material-Only Supply
For experienced in-house maintenance teams and international buyers, PumaCRETE also ships material-only with written installation manuals, video training, and remote technical support. This option is common for federal facilities with in-house contracting authority and for Caribbean and Latin American projects where freight cost favors local labor.
How the Certified Network Works
Every certified installer completes hands-on training at the factory plus field certification on each chemistry family they install. Installer certifications are reviewed annually. The manufacturer warranty only applies to installations performed by an active-certified crew — which is why we take certification seriously and don't sell to uncertified buyers for retail markup.
Project Sizes & Schedules
The network handles single-room rebuilds (under 1,000 square feet, often completed in a long weekend) up to whole-plant installations (50,000+ square feet, phased over multiple shutdown windows). Most projects deliver a written specification and budget within five business days of a site assessment, and break ground within 30 days for typical schedules.
Sector-Specialized Crews
Different sectors need different crew expertise. Cleanroom installations require ISO-classified clean-side staging and particulate-control discipline. USDA meat-plant projects need crews comfortable with sanitary cove detailing and operating-plant phasing. Munitions facilities need crews cleared for explosives-area work. Our project managers route each job to the right specialist.
Documentation & Quality Control
Every installation includes pre-pour substrate moisture testing per ASTM F2170, calibrated mil-thickness measurement during application, and post-cure surface resistance verification for ESD systems. The complete data package is delivered at handover for your QA records and insurance underwriting.
Tolerates 25 lbs of Vapor Pressure
PumaCRETE 300 and 400 series urethane concrete flooring systems withstand up to 25 lbs of vapor pressure through the concrete slab without delaminating, blistering, or cracking. Most competitive industrial floor coatings are rated under 5 lbs — five times less tolerance for the moisture conditions that destroy ordinary epoxy in coastal, food processing, and humid manufacturing environments.
Installs in Operating Coolers Down to 35°F
Cures down to 35°F, allowing installation in active walk-in coolers, refrigerated cellars, dairy cold storage, brewery cold rooms, and outdoor applications. Most competing urethane concrete flooring and epoxy floor coatings require ambient above 60°F — meaning costly refrigeration shutdown during install.
Thermal Shock from -40°F to 248°F
PumaCRETE's coefficient of thermal expansion matches concrete. The urethane concrete system handles thermal swings from blast freezers at -40°F to boiling 212°F wash-downs without delaminating — the failure mode that destroys epoxy floor coatings in food plant floor, brewery, and aerospace applications.
Permanent Integral Slip Texture
Aggregate is integral to the urethane mortar — not a sacrificial broadcast on the surface. The non slip, non skid, and anti slip texture is maintained throughout the full floor thickness, so traction doesn't wear off as the floor sees forklift, foot, and cart traffic. OSHA 1910.22 compliant. Tunable 0.6 to 0.9 coefficient of friction.
Why PumaCRETE Outlasts Competing Industrial Floor Coatings
Specific Reasons Urethane Concrete Survives Where Ordinary Epoxy Fails
Every industrial flooring manufacturer claims “durable” and “chemical resistant.” PumaCRETE’s published technical data shows exactly where competing systems fail — and exactly where urethane concrete flooring, polyurethane cement flooring, and PumaCRETE industrial floor coatings keep performing for 20+ years.
Bonds to Damp Concrete
PumaCRETE 300 and 400 series bond directly to damp concrete substrate — eliminating the long substrate-drying delays that plague conventional epoxy floor coatings. Critical for renovation projects, coastal facilities, and any plant on a tight turnaround enviroment.
One-Pass Trowel Installation
The 400-series urethane concrete is a single-pass system. One troweled application from primer to finish — no multi-coat schedule, no inter-coat cure delays. Fast return to service measured in hours, not days. Industrial floor repair and food plant flooring rebuilds complete in 24–72 hours per zone.
Standards & Compliance Documentation
Built for the Audits Your QA Team Has to Pass
PumaCRETE industrial floor coatings, urethane concrete flooring, ESD flooring, anti static flooring, sanitary flooring, antimicrobial flooring, and aircraft hangar floor coatings satisfy every major regulatory and audit framework across the industries we serve.
How PumaCRETE Compares
Urethane Concrete vs Epoxy — PumaCRETE vs Ucrete vs Stonhard vs Sikafloor
The industrial flooring market has converged on cementitious urethane as the gold standard for food processing floor, brewery flooring, dairy plant flooring, and heavy industrial applications. The real question isn’t urethane vs epoxy — it’s which urethane concrete flooring system fits your budget, schedule, and support requirements. Here’s how PumaCRETE compares to Ucrete UD200 / HF / MF / DP / HPQ, Stonhard Stonclad UT, and Sikafloor PurCem.
| Factor | Standard Epoxy | Ucrete UD200 | Stonhard Stonclad UT | PumaCRETE 401-HF |
|---|---|---|---|---|
| Service Life | 3–7 years | 20+ years | 20+ years | 20+ years |
| Thickness | 10–25 mils | 1/4 to 3/8 inch | 1/4 to 3/8 inch | 1/4 to 3/8 inch |
| Vapor Tolerance | Under 3 lbs | ~15 lbs | ~12 lbs | Up to 25 lbs |
| Min Install Temp | 60°F | ~50°F | ~50°F | 35°F (coolers) |
| Thermal Shock | Delaminates | Excellent | Excellent | Excellent |
| Support Model | Distributor | Multinational | Single-source | Direct factory |
| Warranty | Varies | Mfr terms only | Mfr+installer | 5-yr full coverage |
Ucrete and UD200 are registered trademarks of Master Builders Solutions / MBCC Group. Stonhard and Stonclad are registered trademarks of Stonhard. Sikafloor and PurCem are registered trademarks of Sika. Comparison data based on publicly available technical data sheets and industry installation experience. Not affiliated with or endorsed by Master Builders Solutions, Stonhard, or Sika.
Nationwide U.S. & International Service Area
Industrial Flooring Contractors & Installers in All 50 States
PumaCRETE serves industrial flooring projects from coast to coast. As a direct manufacturer of urethane concrete flooring, industrial floor coatings, ESD flooring, conductive epoxy systems, antimicrobial sanitary flooring, food plant flooring, and aircraft hangar floor coatings, PumaCRETE supplies material nationwide and connects facility owners with factory-certified independent contractors for turnkey installation. For experienced in-house maintenance teams and international buyers, PumaCRETE also ships material-only with full technical support.
Manufacturing
PumaCRETE manufactures high performance industrial resin flooring and coating systems.
Nationwide Contractor Network
With a nationwide network to serve your flooring needs, PumaCRETE can provided localized assistance in most areas of the country.
On Site Training
PumaCRETE offers expert on site training and assistance for surface preparation and application of our products.
Industries we serve
Floors built for your Industry
Pick your industry to see the systems, specs and projects that fit your plant.
Manufacturing Floors
Heavy-duty, industrial manufacturing floor solutions. Durable, attractive, urethane and polymeric finishes to meet the customized needs of your industry. Our fast-curing options can help provide long-lasting durability and attractive finishes, with a fast turnaround.
Anti Static Floors
PumaCRETE anti-static flooring solutions utilize proprietary ESD epoxy floor and urethane technology. Dissipative floors protect sensitive electronic components; Conductive flooring protect your Arms, Ammunition, and Explosives (AA&E) areas.
Food and Beverages Floors
PumaCRETE flooring provides a durable, long-lasting solution with our durable and sanitary work surfaces. Flooring is USDA/FDA compliant, slip-resistant, and chemical-resistant. Fast turnaround can be achieved with our fast-curing materials and very low odor options.
Government Projects
Specialty PumaCRETE heavy-duty flooring was developed for the USPS. Screed applied, these products provide high strength, excellent adhesion, and are designed for the ultimate in durability and fast turnaround.
OFFERS
Exclusive Offers from Company
Workhorse Urethane Flooring for Industry
Light - Medium Duty
PumaCRETE® 100/200 Series
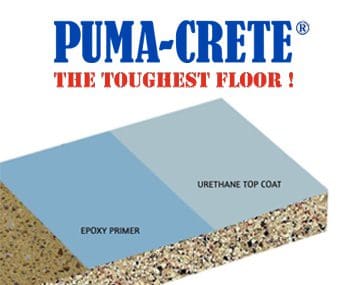
PumaCRETE® 100 series coatings are individual products. A complete coating system, which is a cost-effective light to medium duty solution for your concrete floors in new or “like-new” condition. They are primarily used in dry environments and provide long-lasting protection for your concrete. These multi-layered coating systems provide excellent protection of your facility floor, with an attractive and easy-to-clean finish.
| TRAFFIC | Foot, cart, and occasional power lift usage. |
| THICKNESS | 12 to 60 mils (0.012 to 0.060 inch). |
| HIDING POWER | Increased hiding power for concrete surface defects in renovation projects. |
| FINISH | Satin to gloss. |
| APPLICATION | Spread with a flat or serrated (v-notch) squeegee and rolled with 9- and 18-inch paint rollers. These floors have excellent abrasion resistance for foot and cart traffic, as well as rubber-wheeled power lift traffic. |
| OTHER ADVANTAGES | 1. Good all-around chemical resistance (can be customized for more aggressive chemicals). 2. Customized texture, from smooth as glass to very rough and anything in between. 3. Easy to clean, nonporous finish. |
Heavy Duty
PumaCRETE® 300 Series
PumaCRETE 300® Series is are urethane concrete floor system, customized to your application. They consist of a tough urethane cement base coat with a polymeric top coat or lock coat. The 300 series systems have all-around durability for most heavy-duty industrial traffic conditions. They also offer increased hiding power for concrete surface defects (holes, cracks, rough areas) often found in renovation projects.
| TRAFFIC | Maximum durability for the most abusive environments. Increased thickness increases durability for impact, scraping, and gouge resistance. |
| THICKNESS | 1/16 to 1/4 inch. |
| HIDING POWER | Increased hiding power for concrete surface defects in renovation projects. |
| APPLICATION | Applied with a combination of serrated (v-notch) squeegee(s) and an optional cam or pin rake. |
| OTHER ADVANTAGES | 1. Tolerance to damp and wet conditions. 2. Thermal shock resistant. 3. Good all-around chemical resistance (can be customized for more aggressive chemicals). 4. Texture can be customized for your needs, from smooth as glass to very rough and anything in between. 5. Easy to clean, nonporous finish. |
Extreme Duty
PumaCRETE® 400 Series
PumaCRETE® 400 series is are extra heavy-duty, seamless system. Known as a hand-troweled urethane mortar or screed. Applied at 1/4- 3/4 inch thickness, these were developed for the ultimate durability in punishing environments.
| TRAFFIC | Maximum durability for the most abusive environments. |
| THICKNESS | 1/4 to 1/2 inch. |
| HIDING POWER | Increased hiding power for concrete surface defects in renovation projects. |
| FINISH | Matte/flat. May be waxed for a high-gloss appearance. |
| APPLICATION | Spread and finish with a concrete finishing trowel in one pass (option: spread with a rake or screed box). |
| OTHER ADVANTAGES | 1. One-pass system: can restore badly worn concrete surfaces in as little as one day. 2. Withstands heavy traffic loads, including heavy wheeled carts and fork trucks. 3. Push, pull, drag or drop on this floor: it is difficult to damage this beast. 4. Fast curing: handles heavy cart traffic in as little as 12 hours at 70°F. |
All Duties - ESO
Puma-ESD Series
PumaCRETE® has a complete line of ESD and conductive flooring systems from the 100 to 400 series, called PumaESD. The products include thin film coating systems, hi-build coating systems, and heavy-duty toppings. These systems are customized for the specific needs of each customer. Typical usage includes electronics manufacturing and storage, AGV, AMR and Robot areas, as well as munitions and hazardous volatile chemical processing and storage. Versions feature a four-component, chemical-resistant, aliphatic polyester ESD urethane top coat.
PumaESD Systems are available in conductive (C) or static dissipative (SD) versions and feature reliable electrostatic control properties.
| TRAFFIC CONDITIONS EXPECTED | Options are available for all traffic conditions. |
| THICKNESS | Applied from 12 mils to 1/4 inch. |
| HIDING POWER | Thicker systems provide enhanced hiding of concrete surface defects. |
| FINISH | Satin to semi-gloss. |
| APPLICATION | Applied with serrated (v-notch) squeegee(s) and an optional cam or pin rake. |
EXPERIENCE AND EXPERTISE
THE PumaCRETE Difference
We have over 30 years of experience behind us. Customers can rest assure that the system we recommend shall be the most cost effective. We provide customized solutions for challenging issues.