Detonators & Primers Flooring
Conductive epoxy flooring systems engineered for detonator cap, blasting cap, cartridge primer, percussion primer, and shock-tube detonator production. The highest-volume end of initiator manufacturing with tight resistance control for primary explosive chemistry.
GET A FREE QUOTE

Flooring Built for Detonator and Primer Production
Detonators and primers sit at the start of nearly every explosive train in use — from the primer that fires a cartridge round, to the blasting cap that initiates a stick of dynamite, to the shock-tube detonator in a modern commercial blasting system. Primary explosive chemistry (lead azide, lead styphnate, DDNP, mercury fulminate) is engineered to be sensitive to very low initiating energy.
PumaCRETE® specifies detonator and primer plant floors to the tighter end of the conductive range, with grounding grids suitable for primary explosive handling. The 200 Series conductive epoxy is standard; the 301 Series handles bulk operations and finished-product staging.
This page sits under Initiators & Detonators
Standards & Compliance Framework
Detonator and primer production is governed by DoD manuals on the military side and ATF licensing plus NFPA codes on the commercial side.
DoD 4145.26-M
Contractors’ Safety Manual. Military detonator and primer contractors.
ATF 27 CFR Part 555
Commerce in Explosives. Federal licensing for commercial detonator and primer manufacturers.
SAAMI Guidelines
Sporting Arms and Ammunition Manufacturers’ Institute. Commercial cartridge primer manufacturing practices.
IME SLP-22
Institute of Makers of Explosives. Detonator and initiator manufacturing practices.
ANSI/ESD STM7.1
Floor Materials — Resistive Characterization. Verification test method.
Technical Requirements Detonator Flooring
Primary explosive chemistry drives tighter resistance targets than general AA&E work.
| Property | Requirement | Reference |
|---|---|---|
| Resistance to Ground | 25,000 ohms – 400,000 ohms (tuned low) | DoD 4145.26-M + primary explosive practice |
| Body Voltage Generation | < 50 V in primer rooms | ANSI/ESD STM97.2 |
| Point-to-Point Resistance | < 1.0 × 10⁶ ohms | ANSI/ESD STM7.1 |
| Spark Behavior | Non-sparking; no exposed ferrous aggregates | NFPA 495 |
| Chemical Resistance | Lead azide, lead styphnate, DDNP, cleaning solvents | Facility-specific |
| Seamless Construction | Monolithic — primer dust must not accumulate | Facility best practice |
| Cleanability | Decontaminable between composition changes | Facility SOPs |
| Grounding Grid | 1,000 sq ft typical in primer rooms | PumaCRETE engineering practice |
Primary explosive note
Lead azide, lead styphnate, DDNP, and mercury fulminate are classified as primary explosives — they can be initiated by shock, friction, heat, or static electricity. The floor spec is tuned low specifically for this sensitivity class.
The PumaCRETE® System Families
Two product families cover the full DoD and explosives pillar. Each sub-industry page specifies the system most often used for that application; the three families below are the common foundation.

PumaCRETE 200-PumaESD-c
THICKNESS: 13-45 mils enhanced durability for impact and frequent motorized lift traffic, or restoration of damaged concrete surfaces)
Mid-build conductive epoxy coating. Primer rooms, igniter assembly, pyrotechnic mixing, lighter-duty cartridge production.
Target Resistance
25,000 ohms – 1.0 × 10⁶ ohms
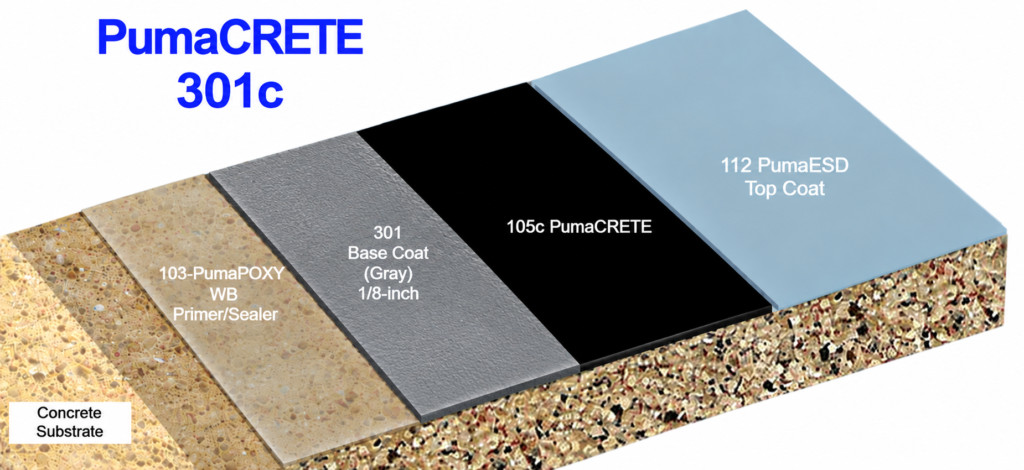
PumaCRETE 301-PumaESD-c
THICKNESS: 1/8 inch (enhance durability for impact and frequent motorized lift traffic, or restoration of damaged concrete surfaces)
Heavy-duty 1/4″ conductive urethane cement topping. Rocket motor casting, LAP lines, artillery production, DoD magazines, mine stores.
RESURFACER ADVANTAGES
Enhanced durability for impact and frequent motorized lift traffic, or restoration of damaged concrete surfaces.
Custom resistance tuning:
For Class 0 initiator work and the most sensitivity-critical operations, PumaCRETE can tune systems as low as 400,000 ohms with charge-generation under 20 volts. Contact our engineering team for a facility-specific recommendation.
Detonator and Primer Operations
PumaCRETE serves military, commercial, and industrial detonator and primer manufacturing.
Detonator & Blasting Cap Production
Commercial blasting caps, non-electric shock-tube detonators, and electric detonator production for mining, construction, and demolition markets.
Cartridge Primer Manufacturing
Boxer, Berdan, and shotgun primer production — the commercial-ammunition end of the primer market under SAAMI guidelines.
Percussion & Specialty Primers
Percussion primers for artillery, specialty primers for aerospace EEDs, and legacy-ammunition primer production.
Shock-Tube Detonators
Nonel-type shock-tube detonator production — a modern blasting-industry product line with specific manufacturing requirements.
Why Detonators Need the Tightest Floor Spec
ESD-dissipative floors (106–109 ohms) protect electronic components. Conductive floors (25,000–106 ohms) protect propellants, primers, initiators, and the personnel handling them. The two are not interchangeable, and the conductive range is what every DoD, NFPA, and ATF framework in this pillar converges on.
Dissipative
106–109 ohms. Protects electronics. Not sufficient for explosives work.
Conductive
25,000–106 ohms. Protects personnel, product, and facility. Required for all DoD and explosives work.
Installation, Grounding & Field Testing
Delivering the specified resistance envelope is a system problem — floor material, substrate preparation, grounding network, and verification testing all have to work together. PumaCRETE installs through a nationwide network of factory-trained crews.
Surface Preparation
Concrete is diamond-ground or shot-blasted to CSP 3–4. Cracks and spalled joints are repaired. Moisture-vapor transmission is tested per ASTM F1869 and F2170. Residual primary explosive composition must be removed from existing floors before coating — this is a safety requirement, not just a surface-prep step.
Grounding Network
Conductive grounding strips are embedded at columns or designated ground points every 1,500 square feet, bonded to the building's earth ground. For sensitivity-critical areas we specify a tighter 1,000-sq-ft grid.
Compliance Verification
- ▸Resistance to Ground — tested per ANSI/ESD STM7.1 using a 100V megohmmeter on a grid pattern.
- ▸Point-to-Point Resistance — verified between randomly selected locations.
- ▸Documentation — full test report for the facility safety file and DoD / ATF / OSHA audit record.
Frequently Asked Questions
Initiators & EEDs FAQ's
A primary explosive is one that can be initiated by shock, friction, heat, or static electricity rather than requiring a dedicated initiator. Lead azide, lead styphnate, DDNP, and mercury fulminate are the common primaries in modern detonators and primers. Their sensitivity drives tighter floor-spec requirements than secondary (bulk) explosives.
Yes. PumaCRETE conductive systems meet the resistance range, non-sparking construction, and seamless-finish practices referenced in SAAMI guidelines for commercial cartridge primer production, as well as the ATF Part 555 licensing requirements that commercial primer manufacturers operate under.
Yes. Both sides of the market share the engineering baseline. Commercial blasting-cap and detonator manufacturers are governed by ATF and NFPA; military detonator contractors by DoD 4145.26-M. The floor system is the same.
Shorter discharge paths. The 1,000-sq-ft grid in primer rooms (vs. 1,500 sq ft in production) provides more frequent ground points around operations handling primary explosive composition, reducing the maximum charge path length.
Yes. PumaCRETE conductive epoxy systems are chemically resistant to the primary explosives used in modern detonator and primer production. The seamless monolithic finish is as important as the chemistry resistance — primary explosive dust must not accumulate in joints.
Yes, sectionally. The 401-ECO fast-cure system allows one bay at a time with 12-hour return-to-service. Commercial primer manufacturers typically phase around annual safety audits.
Yes. ANSI/ESD STM97.2 body-voltage generation testing with the facility's standard footwear is added to standard STM7.1 resistance mapping for primer and detonator installations.
At least annually, and after any floor repair, chemistry change, or significant operations modification. Primary explosive handling warrants more frequent verification than general AA&E.
EXPERIENCE AND EXPERTISE
Specify PumaCRETE for Your Detonator or Primer Facility
Commercial blasting cap plant, cartridge primer line, shock-tube detonator production, or percussion primer manufacturing — PumaCRETE engineers the floor to the primary-explosive sensitivity envelope your operation requires.