Beverage · Bottling & Canning
Beverage Bottling Floors for Syrup Rooms, Fillers and Packaging
Bottling plants run wet, sweet and fast. Syrups and concentrates spill in the syrup room, fillers overflow with sugary product, CIP flushes hot caustic and acid, and broken glass and conveyor chain grind the floor at the line. PumaCRETE urethane concrete flooring resists sugar attack, acids and CIP chemistry, and stands up to forklift and line traffic 24/7.
Sugar
Sealed out of the concrete
9,500 psi
Compressive strength
0.06 g
Abrasion loss (ASTM C501)
5-yr
Written warranty
GET A FREE QUOTE

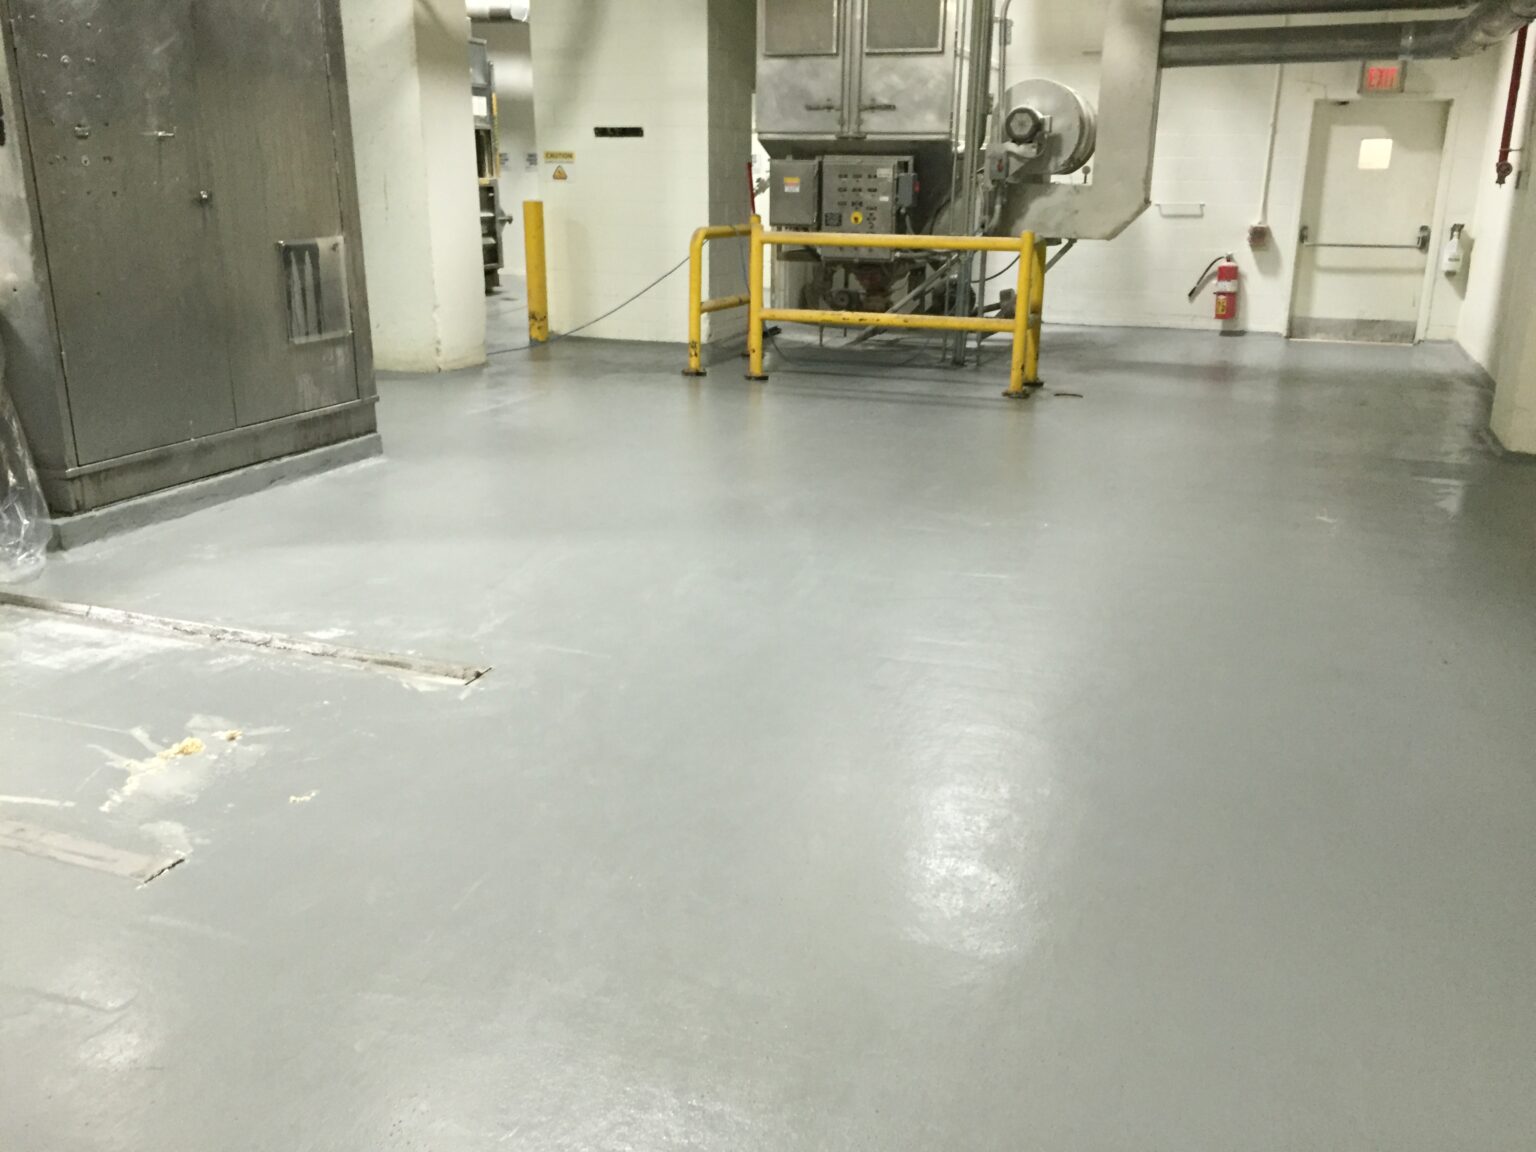
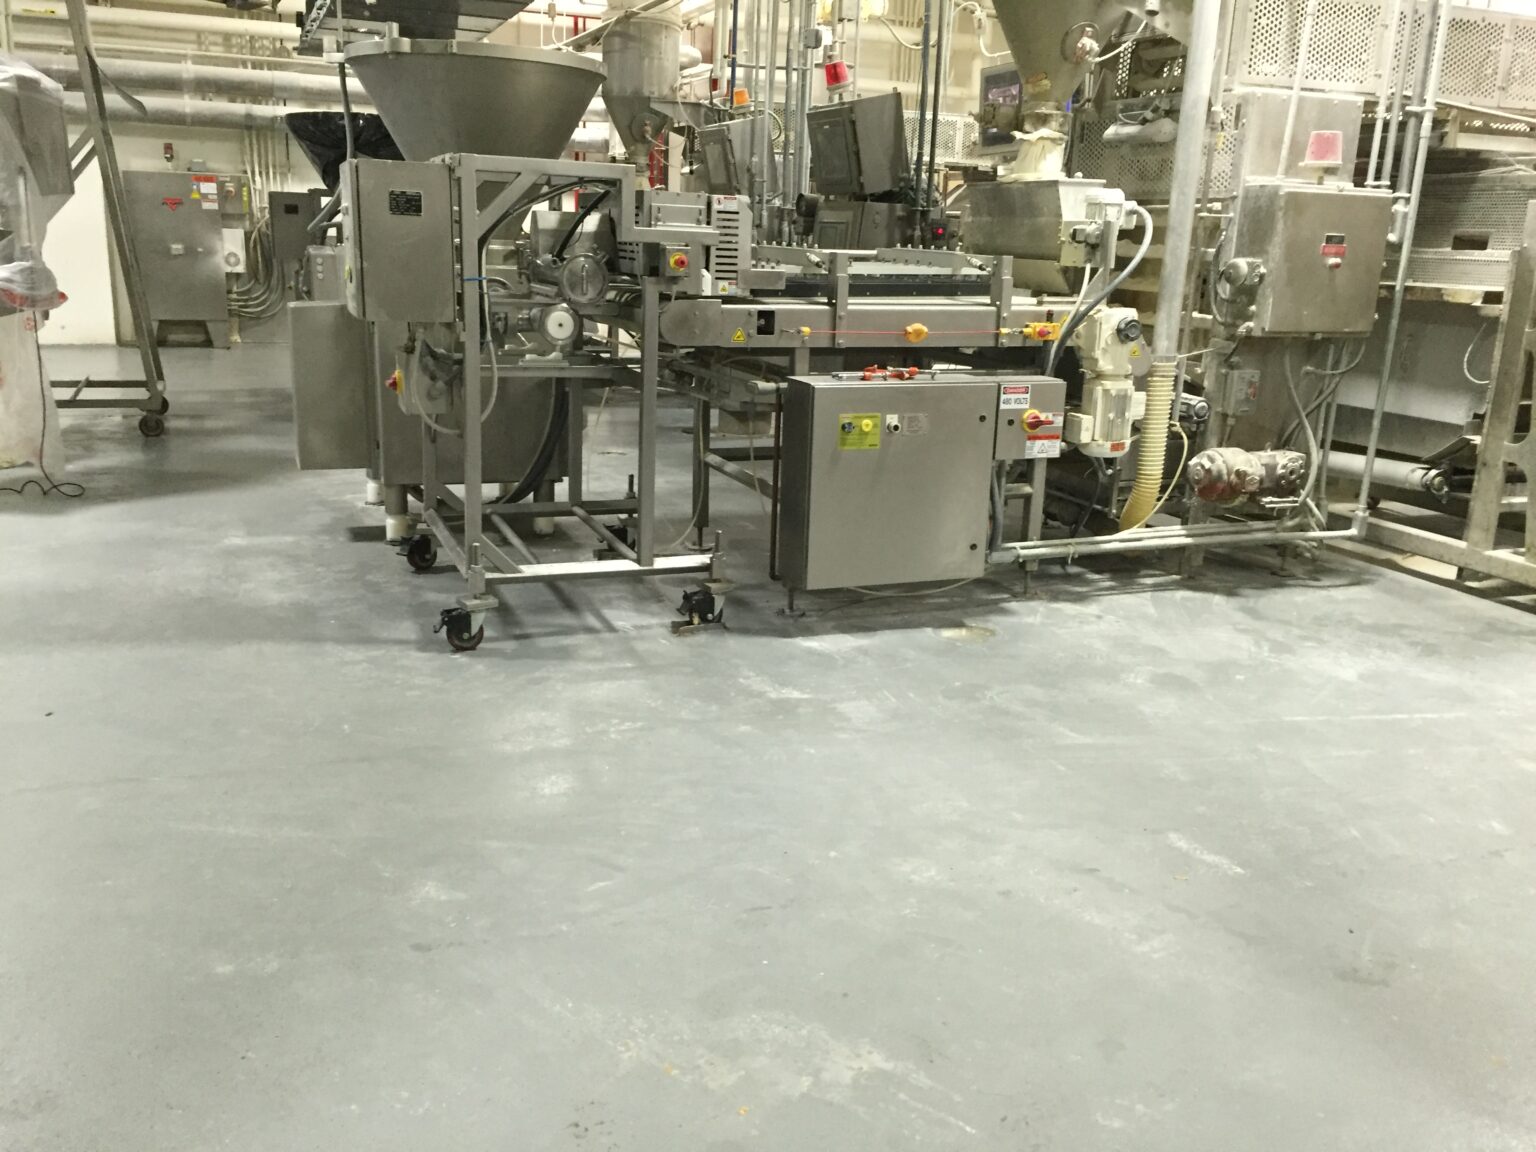
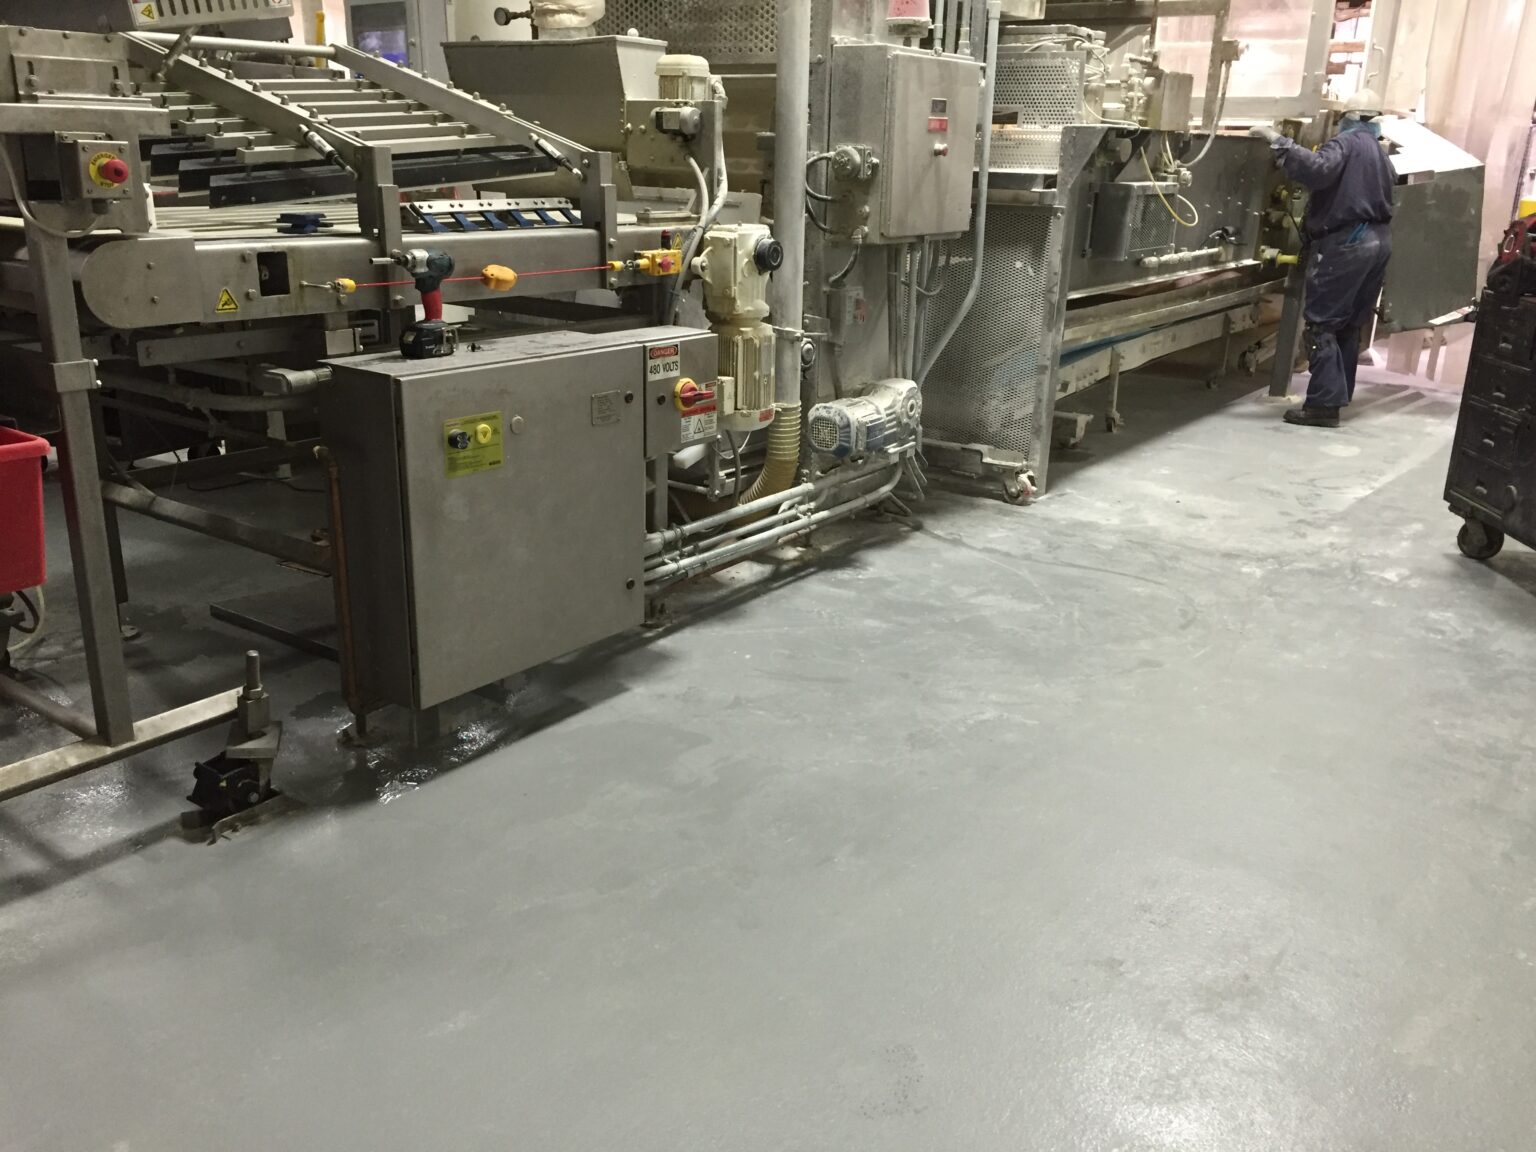
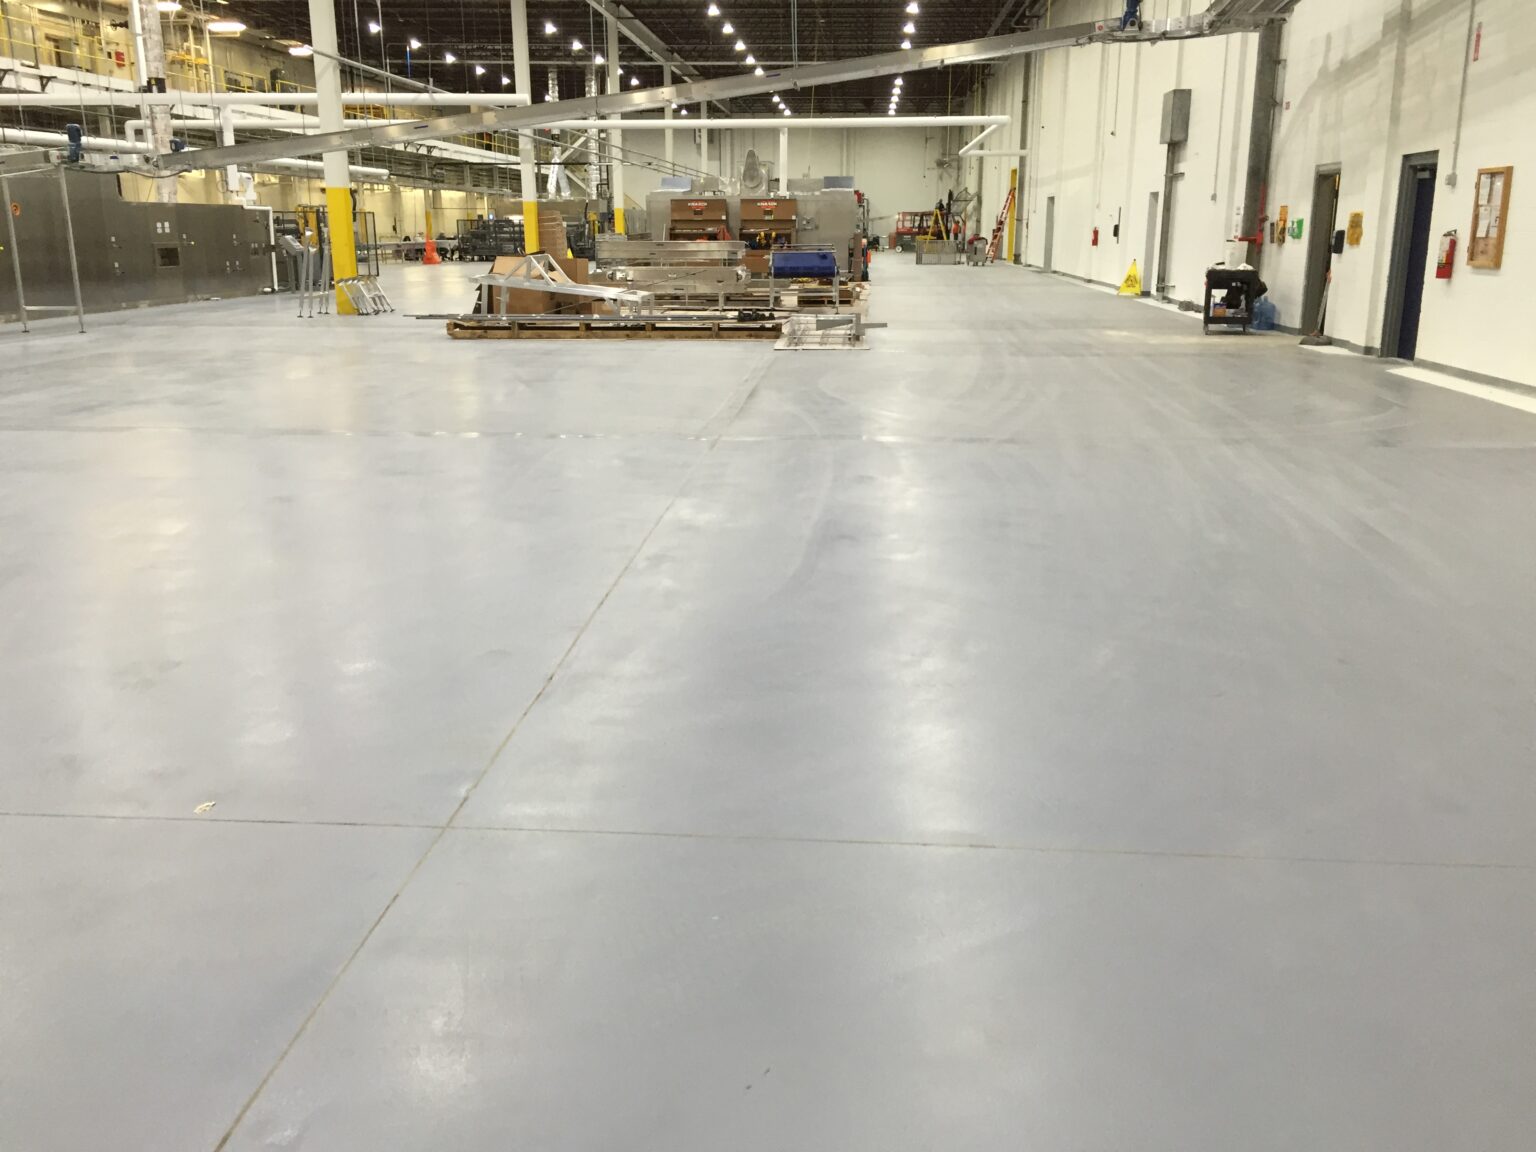
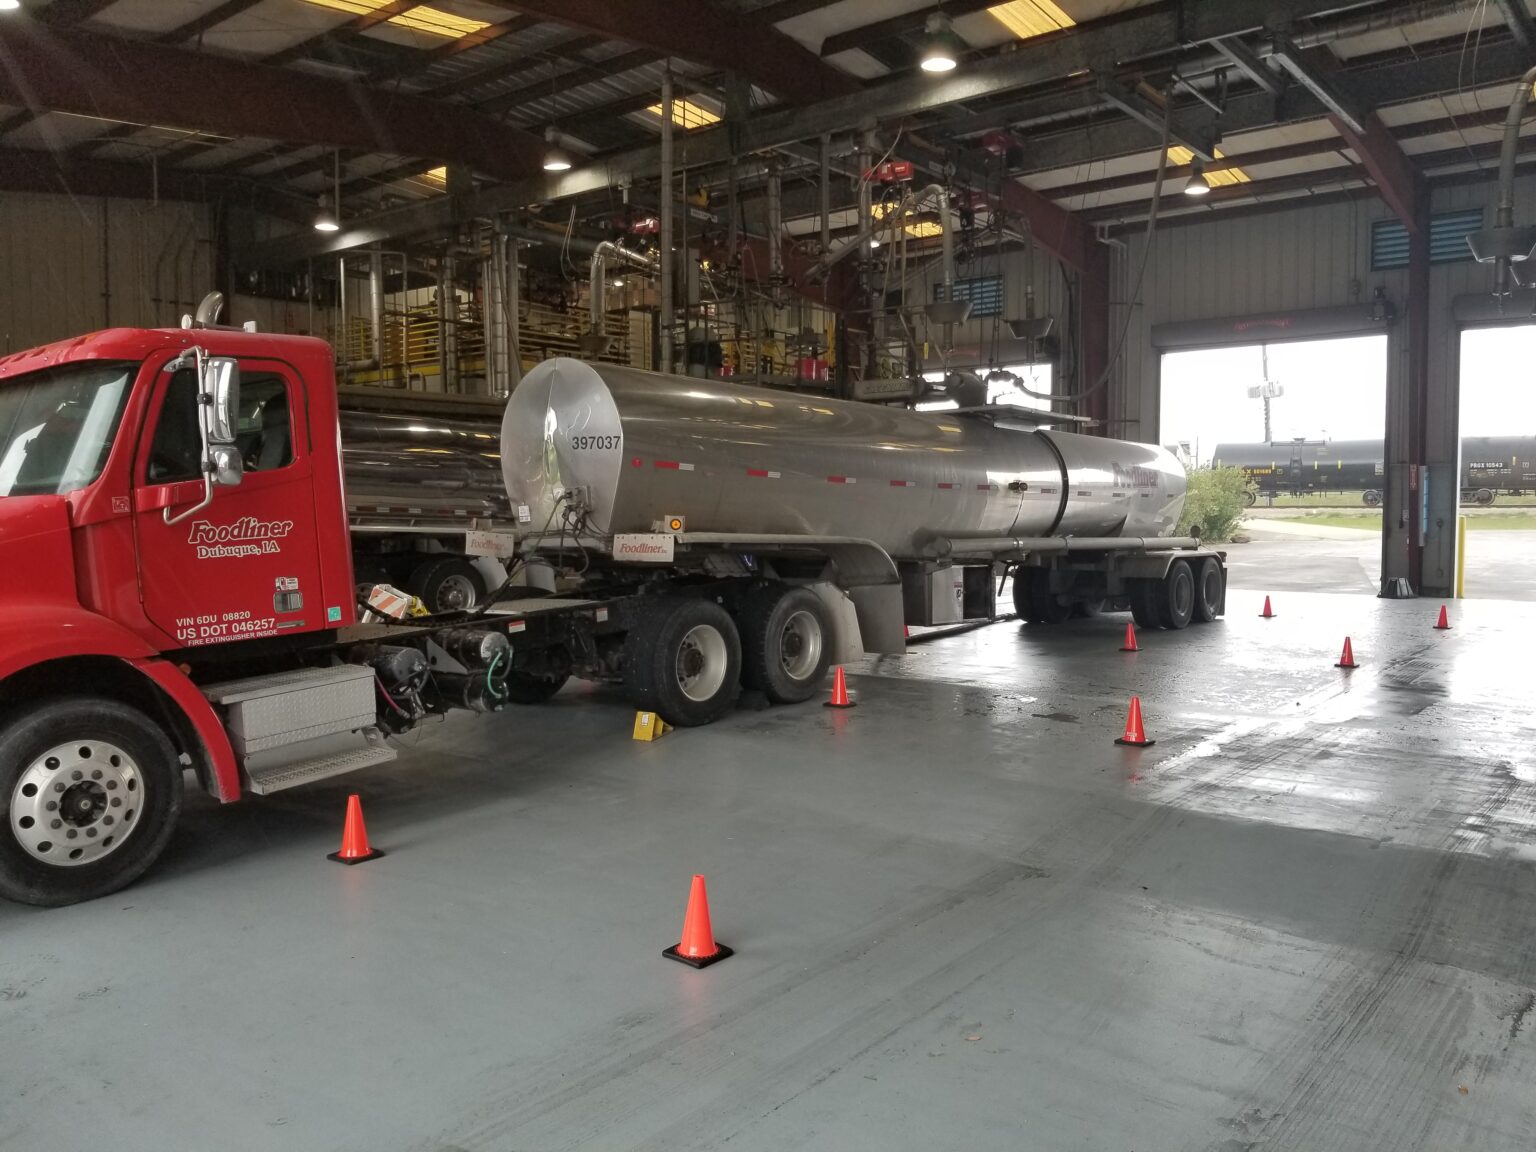
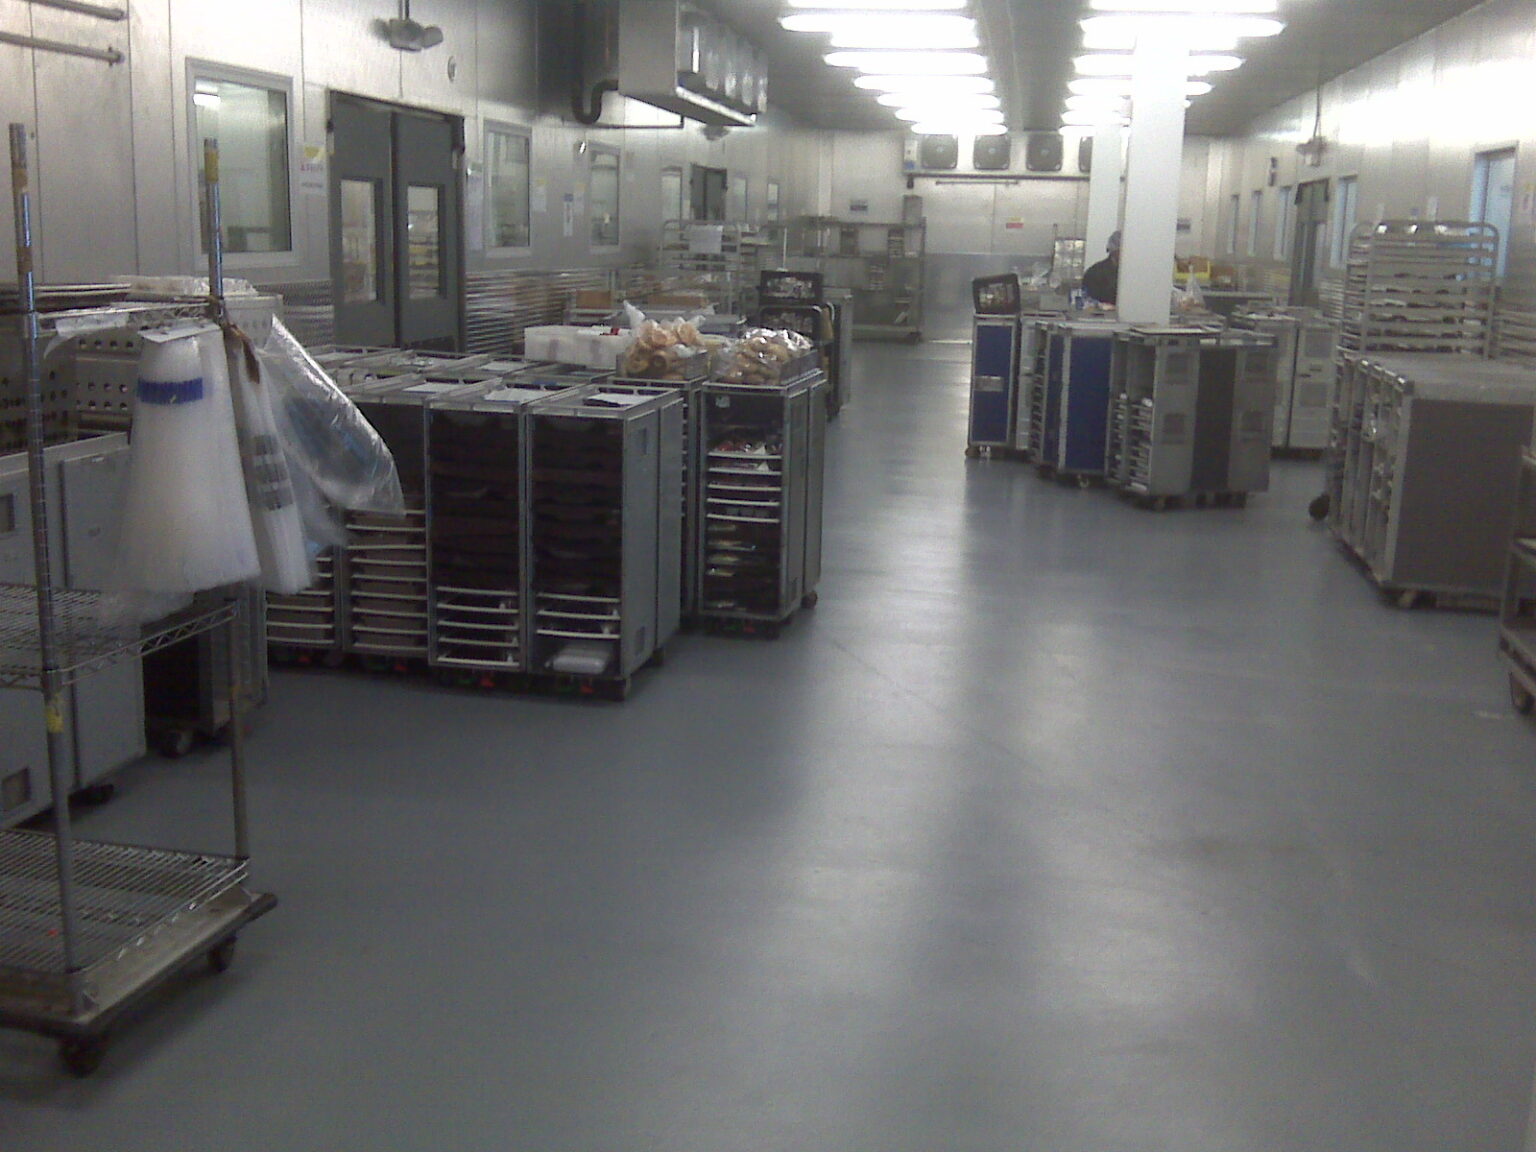
What a bottling plant does to a floor
Sugar attack
Sugar solutions react with the cement in concrete and break it down. A sealed urethane concrete topping keeps syrups and sweetened product out of the slab.
Acidic beverages
Citric, phosphoric and other acids in soft drinks, juices and energy drinks etch concrete and stain coatings. PumaCRETE is formulated to resist food acids.
CIP and sanitation
Blend tanks, fillers and lines are cleaned with hot caustic and acid. Discharge runs to floor drains every shift.
Glass and line abrasion
Broken glass, cans, chain lube and conveyor debris scrape the floor at fillers and packers. Abrasion loss of 0.06 g (ASTM C501) means slow wear.
Forklift traffic
Pallets of empties in, finished goods out, all day. The 9,500 psi system resists wheel wear and impact at turns and doors.
Constant wet at the filler
Fillers and rinsers keep the floor wet for the whole shift. Slip-grade texture keeps footing secure for operators.
Recommended system by zone
One urethane concrete system, configured for the room you’re standing in. Thickness, texture and cove are set zone by zone. Add 1/8 in for integral cove.
| Zone | Recommended system | Key exposures |
|---|---|---|
| Syrup and sugar dissolving room | 401-HF, 1/4 in + cove | Sugar, concentrates, hot water |
| Blend tanks and batching | 401-HF, 1/4 in + cove | Acids, CIP caustic, spills |
| Filler, rinser and capper | 401-HF, 1/4 in, slip-grade | Constant wet, sugary product, glass |
| Hot-fill and pasteurizer tunnels | 401-HF, 3/8 in (thermal) + cove | Hot water, steam, thermal shock |
| Labeling and packaging | 401-HF, 1/4 in | Conveyor debris, cart traffic |
| Warehouse and dock | 401-HF, 1/4 in | Forklift traffic, wheel wear |
Installing around line changeovers
Line by line
Lines are done during planned shutdowns, with the rest of the plant in production.
Under and around equipment
The topping is coved up filler and conveyor stands so sugary product can’t collect at the base.
Drains and trenches
Trench drains at fillers are rebuilt and edged so sugar water doesn’t undermine the slab.
Food safety and audits
- Meets FDA current good manufacturing practice: floors that can be adequately cleaned and kept in good repair (21 CFR Part 117)
- Bottled water plants: supports the plant sanitation requirements of 21 CFR Part 129
- Aligned with SQF, BRC, IFS and FSSC 22000 audit expectations
- OSHA-compliant slip resistance (wet coefficient of friction 0.6–0.9)
Performance data
| Property | PumaCRETE 401-HF |
|---|---|
| Compressive strength | 9,500 psi (ASTM C579) |
| Tensile strength | 1,450 psi (ASTM C307) |
| Flexural strength | 3,200 psi (ASTM C580) |
| Bond to concrete | Exceeds substrate (ASTM D7234) |
| Abrasion resistance | 0.06 g loss (ASTM C501) |
| Impact resistance | >160 in-lb (ASTM D2794) |
| Service temperature | -40°F to 248°F |
| Thermal shock | Pass, boiling-to-ambient cycles |
| Wet coefficient of friction | 0.6–0.9 (tunable) |
| Vapor pressure tolerance | Up to 25 lbs through the slab |
| Minimum install temperature | 35°F (operating coolers) |
| Standard thickness | 1/4 in (3/8 in in thermal zones) |
Standard 1/4-inch PumaCRETE 401-HF system. Full test data is on the technical data sheets.
Three ways to buy, direct from the manufacturer
Every system on this page is made by PumaCRETE and sold direct, with no distributor markup.
Buy the materials
Urethane concrete, primers, topcoats and cove kits shipped direct from the manufacturer to your plant. No distributor markup.
Buy it installed
Turnkey installation by factory-trained crews, with material and workmanship warranties from a single source.
Train your own crew
A factory-employed PumaCRETE trainer certifies your maintenance team or local contractor on your slab: prep, mixing, troweling, cove and testing.
Frequently Asked Questions
Beverage Bottling FAQ's
Sugar reacts with the compounds in cured cement and weakens the surface over time, especially with constant wetting. A sealed urethane concrete topping keeps sugar solutions away from the concrete.
Yes. We specify 3/8 inch in hot-fill and tunnel pasteurizer areas. The system is rated for service up to 248°F.
Yes. The seamless surface supports the sanitation requirements bottled water plants follow under 21 CFR Part 129.
Most areas return to production about 24 hours after the final coat, with foot traffic at 6 hours.
More Related food & beverage floors
EXPERIENCE AND EXPERTISE
Ready to spec your bottling plant floors?
Get a no-obligation site assessment. We review your rooms, chemistry, temperatures and production calendar, then deliver a written specification and budget within five business days.