AA&E · Munitions · Energetics · Propellants
Conductive Epoxy Flooring
PumaCRETE® conductive epoxy and urethane cement flooring systems engineered for arms, ammunition, and explosives (AA&E) facilities, energetics handling, military munitions, propellant manufacturing, and flammable solvent storage. Compliant with DoD 4145.26-m, NFPA 99, and ANSI/ESD S20.20. PumaCRETE conductive (-c) systems achieve resistance below 300,000 ohms — providing a built-in factor of safety against the 1.0 million ohm DoD ceiling.
GET A FREE QUOTE

The PumaCRETE Buying Experience
Three Ways to Buy. One Engineered Conductive System.
PumaCRETE customizes the buying experience to match how your AA&E or energetics project is structured. Choose complete turnkey installation through our nationwide network of certified applicators, purchase materials only if you have your own crew or contractor (with detailed instructions, videos, specialty tools, and surface prep guidelines included), or schedule expert on-site factory training to qualify your own installers. One manufacturer, three ways to buy.
When the Risk Is Ignition, Not Just ESD
In electronics manufacturing, the goal of an ESD floor is to protect sensitive components from damage. In munitions, energetics, and flammable handling facilities, the stakes are different — a static discharge can ignite an explosive material, fuel vapor, or combustible bulk solid. The handling of these materials can lead to an ignition event, fire, or explosion. Common ignition sources include filling an improperly grounded plastic bucket with xylene, pneumatic filling of a storage silo with combustible bulk solid, or dumping bulk solid out of flexible intermediate bulk containers (FIBCs). Conductive flooring is the engineering control that interrupts this chain.
Per the ANSI/ESD definition, the resistance to ground of a conductive epoxy floor is 25,000 ohms to 1.0 × 10&sup6; (1 million) ohms. Per DoD Manual 4145.26-m, the combined resistance of floor plus footwear plus body must be below 1.0 million ohms. PumaCRETE engineered our conductive (-c) systems with the floor alone achieving below 300,000 ohms — well beneith the regulatory ceiling. This factor of safety means that even after accounting for footwear and body resistance, your facility stays within DoD compliance with margin to spare.
PumaCRETE conductive systems are specified for arms, ammunition, and explosives (AA&E) facilities, military-grade weapons handling, energetics, propellant manufacturing, Solid Rocket Motor (SRM) areas, cartridge and missile assembly, grenade production, aerospace propellant handling, and flammable solvent operations. Reference DoD Manual 4145.26 via DoD ASSIST(opens in new tab) or NFPA 99 via NFPA(opens in new tab).
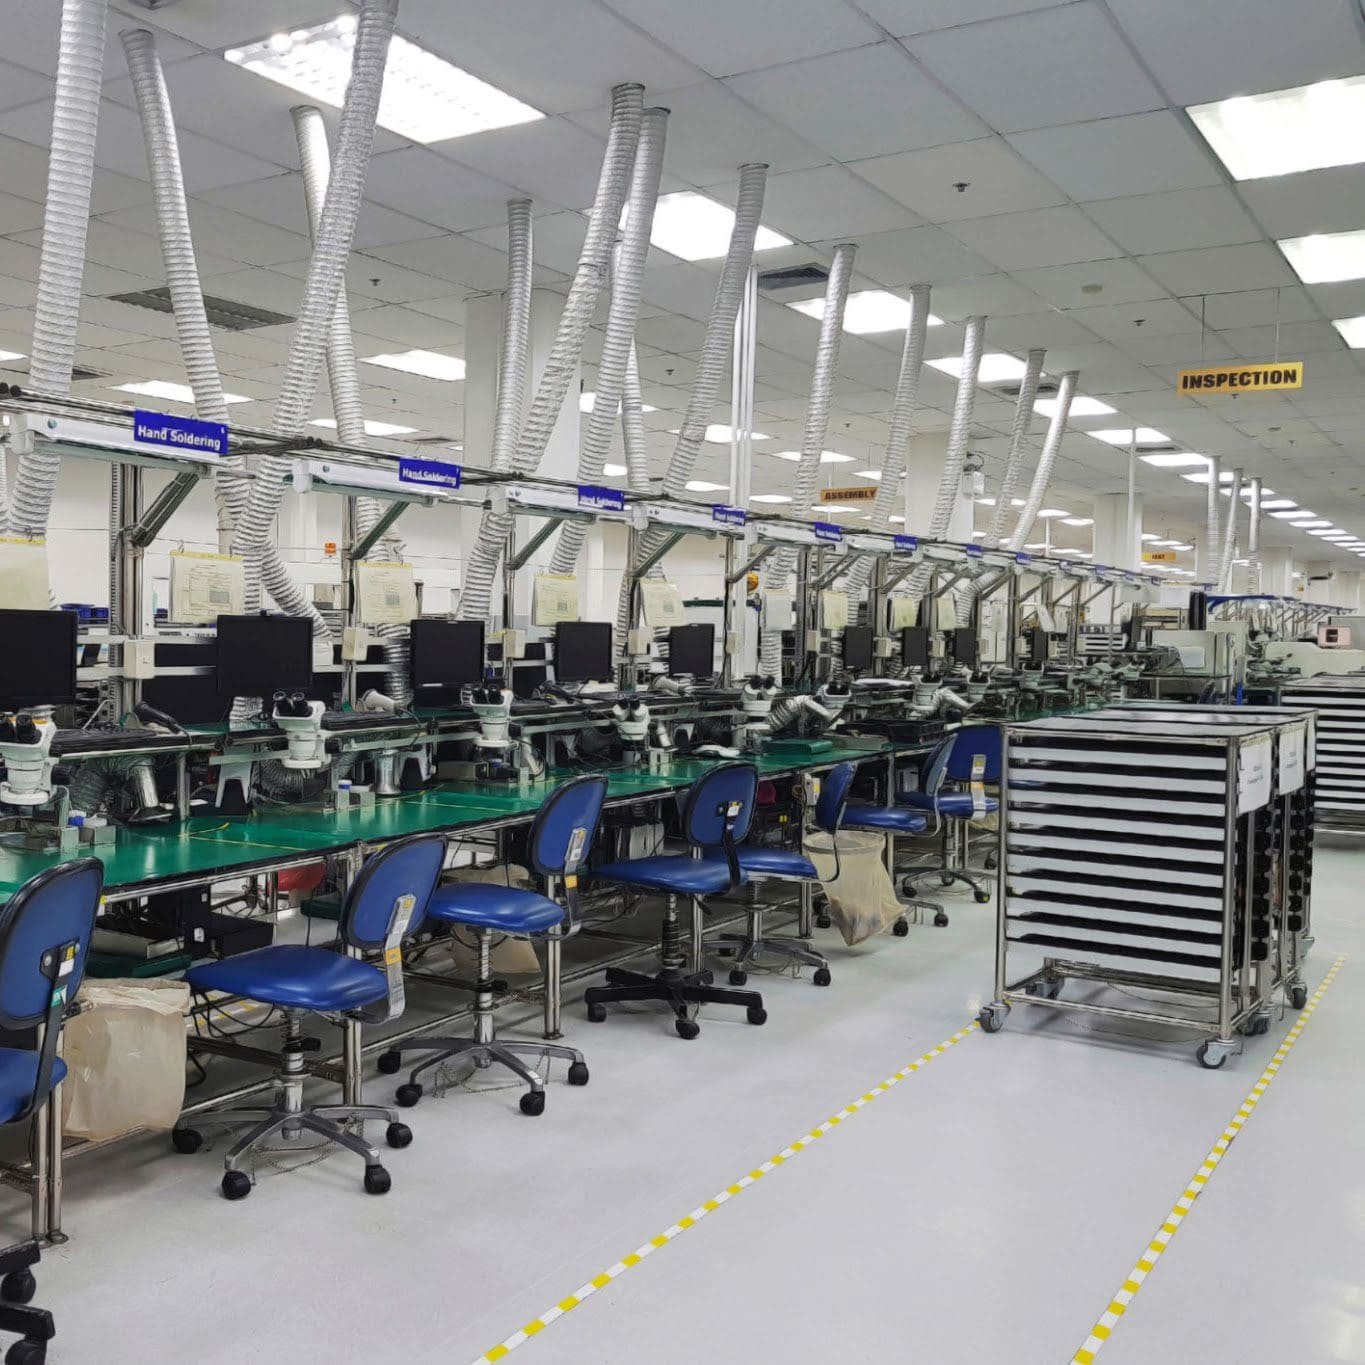
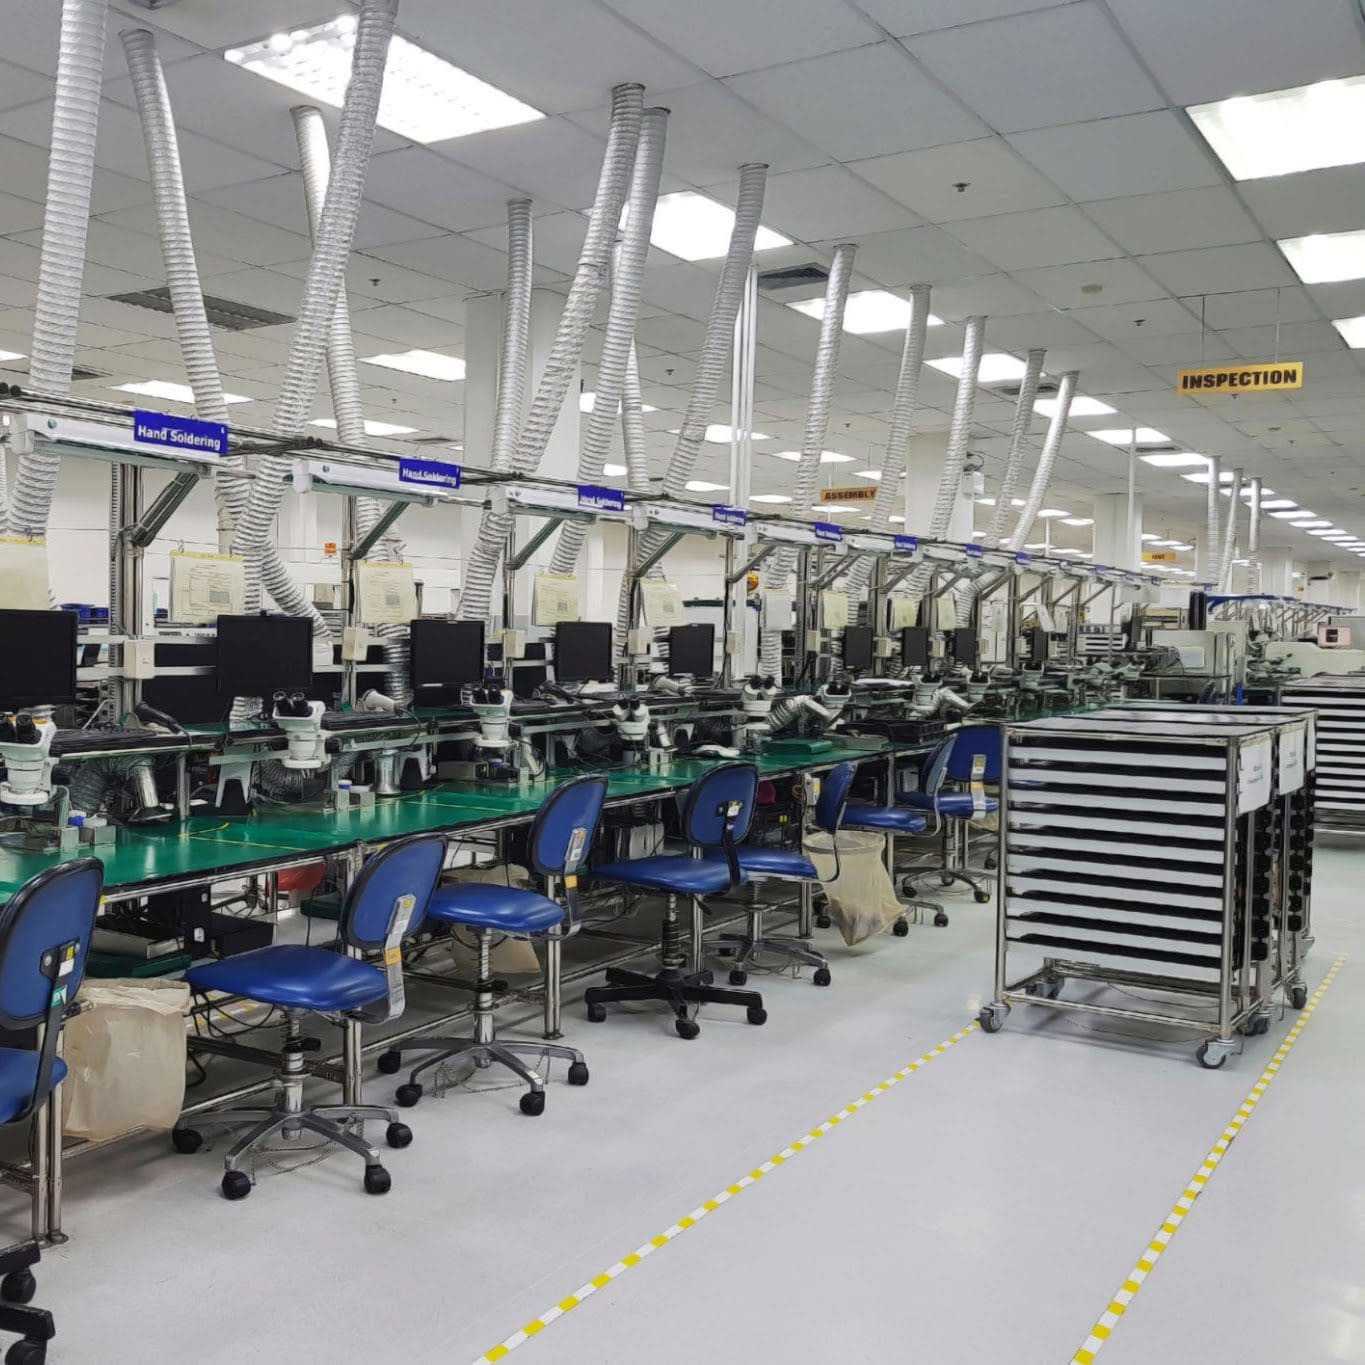
Industry sectors for ESD flooring:
AGV ROBOT AREAS
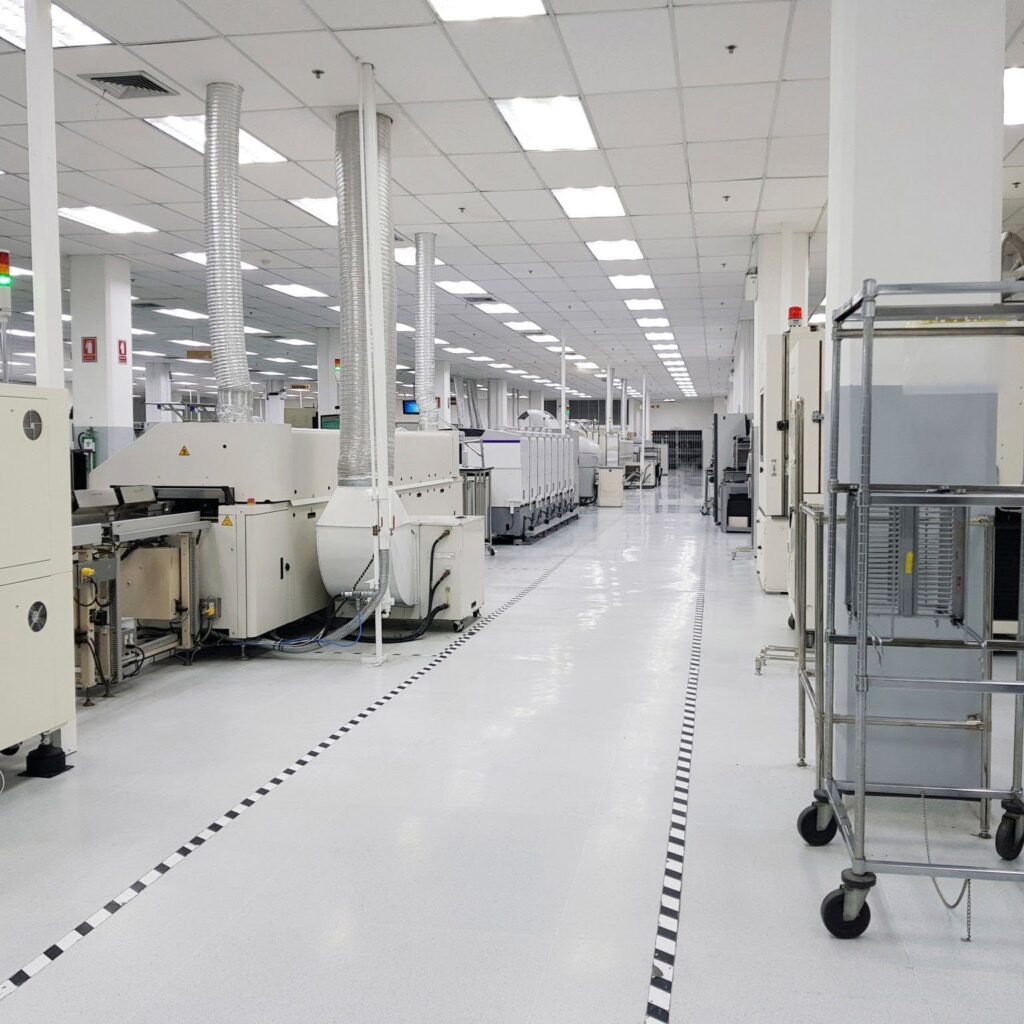
ELECTRONICS MANUFACTURING
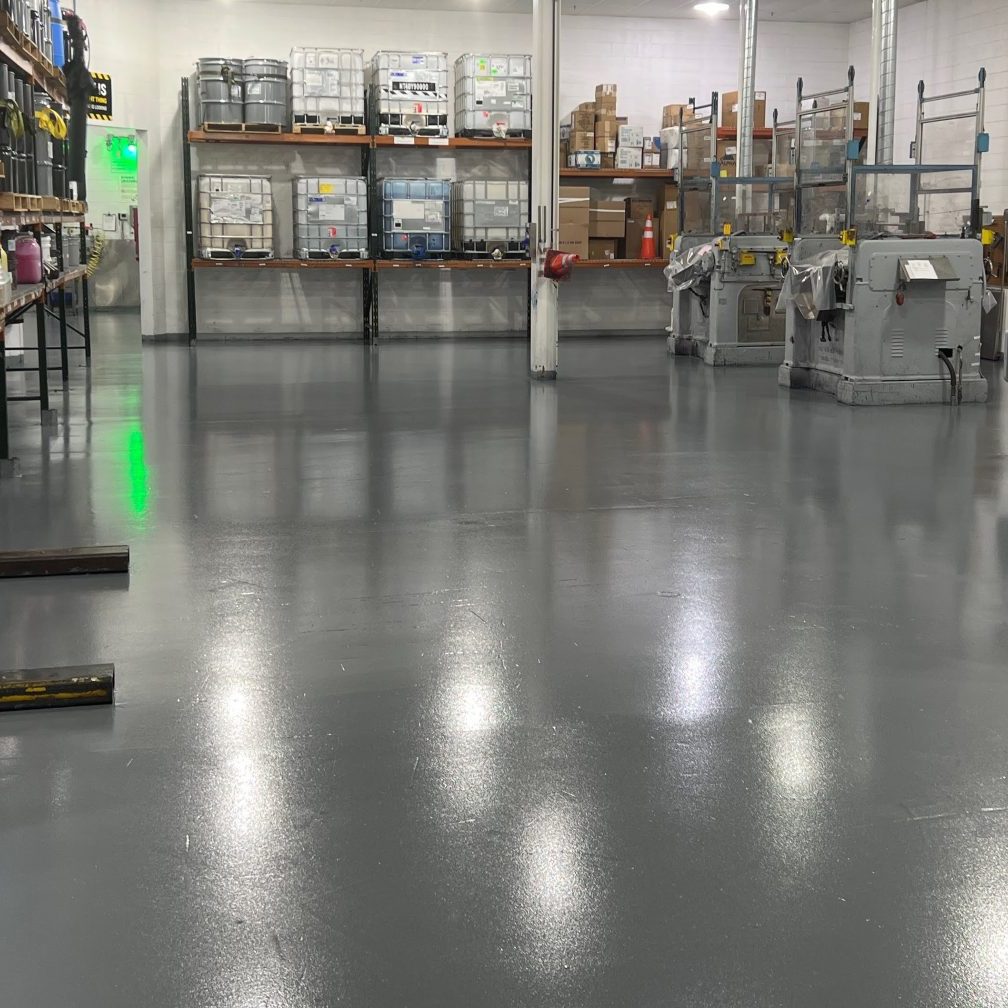
AMMUNITION / EXPLOSIVES
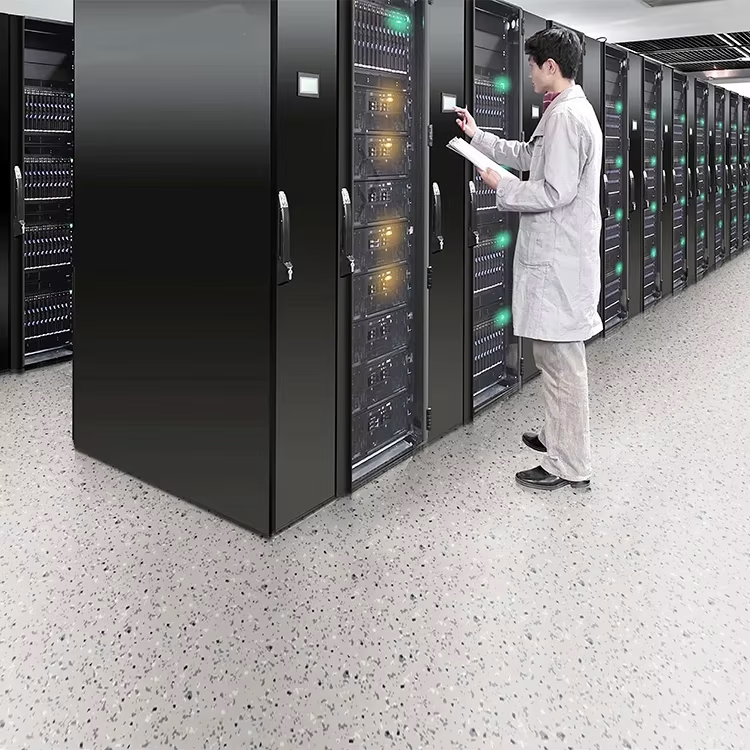
DATA NETWORK CENTERS
Where Conductive Flooring Is Required
Every facility where static ignition could cause a fire, explosion, or unintended initiation of energetic material requires conductive flooring. These are the application areas where PumaCRETE conductive systems are most commonly specified.
AA&E Storage
Arms, ammunition, and explosives storage facilities. Heavily regulated for physical security and accountability. Conductive floor below 300k ohms.
Munitions Assembly
Cartridges, missiles, grenades, mortars. Production lines, kitting, final assembly. DoD 4145.26-m mandatory.
Energetics & Propellants
Energetic material production, propellant casting, Solid Rocket Motor (SRM) assembly. Aerospace and defense propellant handling.
Flammable Solvents
Solvent dispensing, paint mixing, chemical handling with xylene, toluene, MEK, acetone. Prevents static spark ignition.
Combustible Bulk Solids
Silo filling, FIBC dumping, dust-handling operations. Ignition risk from pneumatic transfer of combustible powders.
Aerospace Propellant
Aerospace SRM facilities, satellite propellant handling, spacecraft propulsion assembly.
Healthcare Anesthesia
NFPA 99-governed healthcare anesthesia areas, surgical suites where flammable anesthetic gas was historically used (legacy requirement).
PumaESD Product Lineup
Product Tier Recommendations for Conductive Applications
Graphite micro-particles embedded throughout the PumaESD matrix — not painted on top. ESD performance lasts for the life of the floor, with no wax, no topical recoating, and no maintenance to preserve electrical properties. Every system available in dissipative (SD) or conductive (C) versions.
PumaESD 100-C
Conductive multi-layer epoxy. 12–30 mils. Light-traffic munitions inspection, energetics R&D, smaller AA&E storage rooms on like-new substrate.
Below 300k ohms
PumaESD 200-C
Hi-build conductive epoxy with broadcast aggregate. 30–60 mils. Munitions assembly lines, flammable solvent rooms, fuel handling.
Below 300k ohms
PumaESD 301-C
Multi-layer conductive composite. 1/16″–1/8″. Munitions facilities with material movement, AGV/AMR-equipped energetics operations.
PumaESD 400
Hand-troweled conductive urethane cement mortar. 1/4″–1/2″. Explosives processing, pyrotechnic mfg, SRM, propellant casting. Chemical-resistant.
Conductive (C) standard
Interested in other industries/sectors for ESD flooring?
AGV ROBOT AREAS
ELECTRONICS MANUFACTURING
DATA NETWORK CENTERS
Technical Specifications
Standards-Backed Conductive Performance
PumaCRETE conductive systems meet DoD ASSIST(opens in new tab) Manual 4145.26-m, NFPA 99(opens in new tab), and ANSI/ESD S20.20(opens in new tab). Reference the official DoD Manual 4145.26 whitepaper on conductive flooring for full compliance detail.
| Specification | Conductive Flooring Standard Range | PumaCRETE Achievement |
|---|---|---|
| Resistance to ground | 25,000 ohms to 1.0×10&sup6; ohms | As low as 400k ohms standard |
| PumaCRETE -c version | n/a (factor of safety) | Below 300,000 ohms |
| Combined floor + footwear + body | Below 1.0 million ohms (DoD 4145.26-m) | Meets — with margin |
| Thickness range | n/a | 12 mils to 1/2 inch |
| Service temperature | n/a | -50°F to +250°F |
| Grounding tape spacing | Per ANSI/ESD S20.20 specs | Every 1,500 sq ft + columns |
| Chemical resistance (400 series) | n/a | Resistant to fuels, solvents, oxidizers |
DoD 4145.26-m Compliance Quick Check
The DoD Manual 4145.26-m governs ammunition and explosives ESD protection. Five requirements your conductive floor system must satisfy:
| DoD 4145.26-m Requirement | PumaCRETE Conductive Provides |
|---|---|
| Floor + footwear + body resistance below 1.0 million ohms | Yes — floor alone below 300k ohms |
| Bonded electrical ground | Yes — copper grounding tape every 1,500 sq ft + columns |
| Post-install electrical testing | Yes — included with every turnkey installation |
| Compliance documentation for audit | Yes — written certification delivered |
| Chemical resistance to energetics & propellants | Yes — PumaESD 400 urethane cement |
PumaCRETE Conductive vs. Other Conductive Flooring Manufacturers
Major industrial flooring manufacturers offer conductive products — Stonhard, Dur-A-Flex, Sika, Florock, FlexGard, BASF. The difference is in DoD 4145.26-m factor of safety, urethane cement tier availability, and buying flexibility.
| Capability | PumaCRETE Conductive | Typical Competitor Range |
|---|---|---|
| Floor resistance achieved | Below 300,000 ohms (-c version) | 500k–1.0M ohms typical |
| DoD 4145.26-m factor of safety | Yes — engineered headroom | |
| Often at the ceiling, no margin | ||
| Urethane cement conductive tier | Yes — PumaESD 400, 1/4″–1/2″ | Rare — most stop at epoxy |
| Buying options | Turnkey · materials only · factory training | Typically turnkey only |
| DIY documentation included | Yes — videos, tools, prep guides | Limited / extra cost |
| Post-install testing included | Yes — with turnkey | Often extra-cost service |
Comparison based on publicly published competitor data. PumaCRETE is not affiliated with Stonhard, Dur-A-Flex, Sika, Florock, FlexGard, or BASF. Trademarks belong to their respective owners.
Thin Film Conductive Coatings
ESD Epoxy Flooring System Types
Best for light-duty to medium duty environments and controlled spaces.
FEATURES
- Meet ESD S20.20, DoD4145.26m, NFPA99 requirements.
- Smooth finish (or light texture)
- High abrasion resistance for heavy foot traffic, carts and wheeled loads.
- Easy to clean
- Chemical resistant
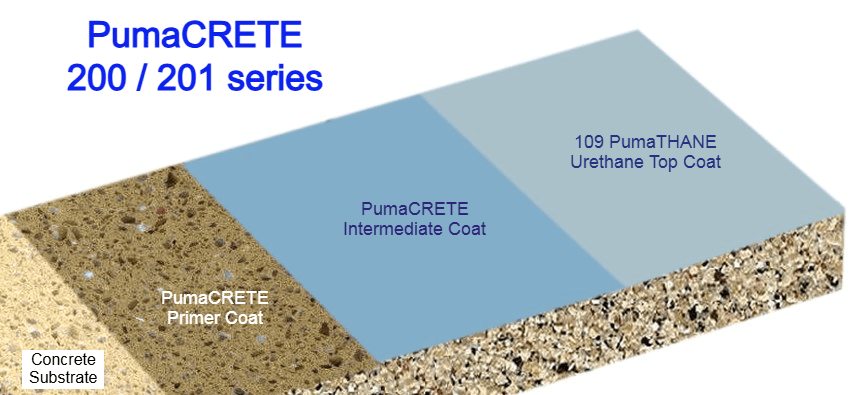
Heavy-Duty Conductive Mortar Systems 1/16 to 1/4 inch
Used in the most demanding environments.
FEATURES
- Restores damaged concrete
- Impact resistance
- High compressive strength
- Extended lifecycle performance
- Meets ESD S20.20, DoD4145.26m, NFPA99 requirements.
- Chemical resistant
Best for medium to heavy duty environments.
- Smooth finish (or light texture)
- High abrasion resistance for heavy traffic including forklifts, rubber and plastic wheels.
- Easy to clean
Installation & Certification
Installed by Factory-Trained Certified Applicators
Every PumaCRETE turnkey installation is delivered by factory-trained, factory-certified applicators working from our nationwide installer network. We do not sub-contract to unknown crews. Every installer has been trained at PumaCRETE on system chemistry, surface preparation, ground grid integration, and post-install ESD resistance testing — and every installation is backed by a manufacturer-plus-installer warranty.
Six-Step Turnkey Process
1. Hazard Assessment & Spec
On-site evaluation. Substrate condition, governing standard (DoD 4145.26-m, NFPA 99, ANSI/ESD S20.20), AA&E or energetic material classification, traffic loads, and grounding plan evaluated. Written spec delivered for facility safety officer review.
2. Ground Grid & Prep
Copper ground straps integrated with building electrical ground. Diamond grinding or shotblasting achieves CSP 3–5 profile. Cracks repaired, joints treated.
3. Surface Prep
Diamond grinding or shotblasting achieves CSP 3–5 profile. Cracks repaired, joints treated. Surface ready to receive conductive primer.
4. Conductive Primer + Floor System
Conductive primer establishes continuity across the floor and connects to the grounding tape grid. Selected PumaESD system applied — conductive epoxy for assembly/storage or PumaESD 400 urethane cement for energetics processing.
5. Cure & Resistance Testing
Post-install resistance testing at multiple grid points, documented against ANSI/ESD S20.20 or DoD 4145.26-m.
6. Certification & Warranty
Written compliance certification for audit records. Manufacturer + installer warranty. Written maintenance protocols for facility sanitation staff.
DIY Materials & On-Site Factory Training
If you have your own crew or contractor, PumaCRETE ships PumaESD conductive materials direct, with detailed installation instructions, videos, specialty tools, surface prep guidelines, and phone/email technical support during the project. Prefer to qualify in-house installers for future projects? PumaCRETE will train your team on system chemistry, surface prep, grounding tape integration, and post-install electrical testing on site. Either way, you stay in DoD 4145.26-m and NFPA 99 compliance.
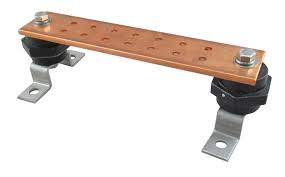
EARTH GROUND (copper ground rod, bar, outlet.
Copper ground rods are often used in Military, Munitions, and manufacturing environments. At the ground point on rod... remove oxidation from rod (for connection with a clamp). Run copper foil tape on the floor, per figure 2. Run the tape up the ground rod, and secure tape to ground rod using the copper foil tape.
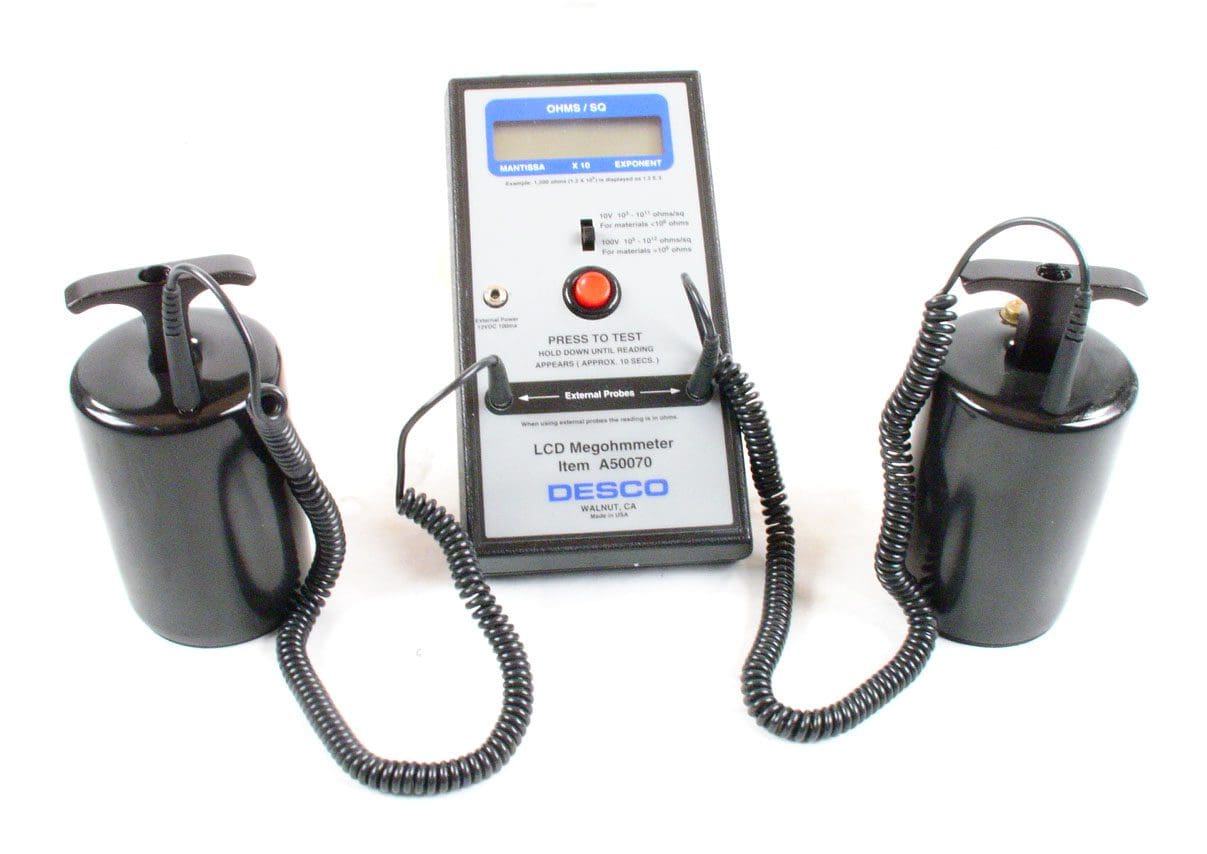
Certify the Flooring meets:
DoD 4145.26M(opens in new tab) ESD Association S20.20(opens in new tab) NFPA(opens in new tab) OSHA(opens in new tab)
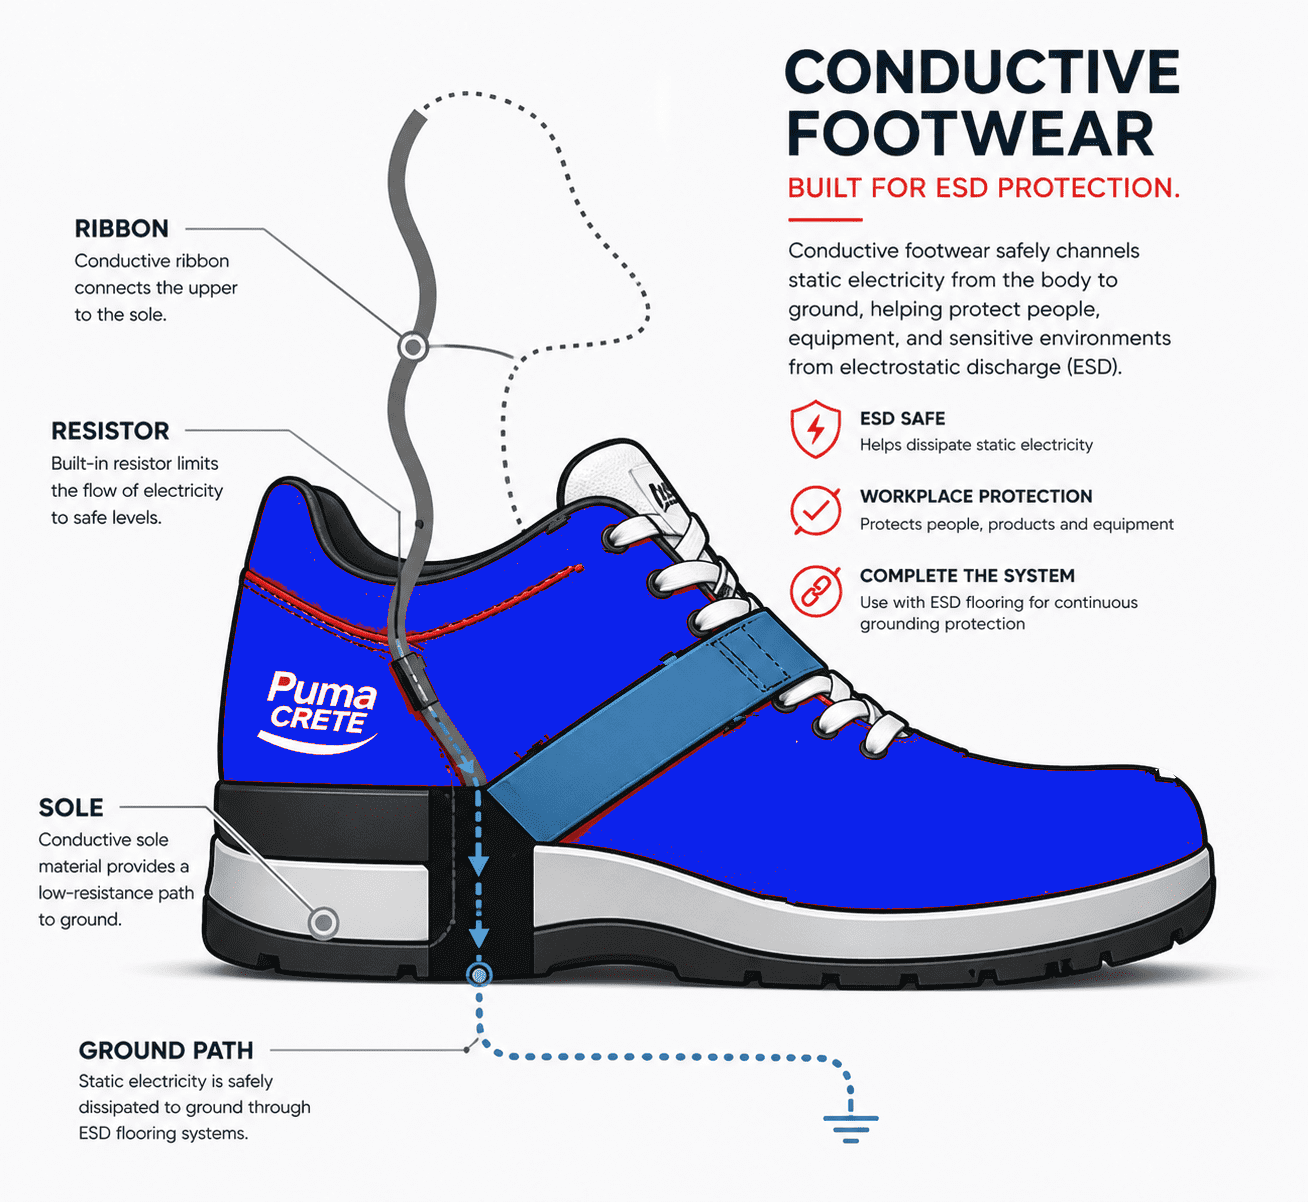
Certify the Flooring meets:
DoD 4145.26M(opens in new tab) ESD Association S20.20(opens in new tab) NFPA(opens in new tab) OSHA
NATIONWIDE NETWORK OF INSTALLATION
With a nationwide network of installers, PumaCRETE® has provides a tradition of quality. Our factory-trained installation crews can provide turn-key installation and localized service. In many cases, we can train your personnel or local contractor, with on site training available.
PumaCRETE® SITE TRAINERS
PumaCRETE® can provide on site trainers, along with detailed installation instructions and videos, specialty tools, and surface prep guidelines for new installers or DIY installation. See our installation page for our application resources.
Frequently Asked Questions
Conductive Epoxy Flooring FAQ
Static dissipative (SD) flooring has resistance between 1×10&sup6; and 1×10&sup9; ohms — high enough to safely bleed off static but low enough to prevent fast discharge that could damage ESD-sensitive electronics. Conductive (C) flooring has lower resistance (25,000 to 1.0 million ohms) and dissipates charge faster. Dissipative is for electronics manufacturing; conductive is specified for AA&E, munitions, energetics, propellants, and flammable solvents where the goal is ignition prevention, not just component protection.
DoD Manual 4145.26-m is the DoD Contractor's Safety Manual for Ammunition and Explosives. It requires the combined resistance of floor plus footwear plus body to be below 1.0 million ohms. PumaCRETE conductive (-c) systems achieve below 300,000 ohms on the floor alone — providing a built-in factor of safety so that the combined floor + footwear + body resistance stays well below the 1.0 million ohm ceiling.
Flammable storage and processing, energetics manufacturing, explosives storage and processing, military munitions (cartridges, missiles, grenades, Solid Rocket Motors), arms and ammunition facilities, propellant handling, aerospace energetic systems, fuel and solvent operations, and any environment where static ignition could cause fire or explosion. Common ignition sources include filling improperly grounded plastic buckets with solvents like xylene, pneumatic filling of silos with combustible bulk solids, and dumping bulk solids out of flexible intermediate bulk containers (FIBCs).
Conductive grounding tape (copper strap) is installed beneath the conductive primer at columns or designated ground points, with one connection point every 1,500 sq ft minimum. The grounding tape is electrically bonded to building earth ground per ANSI/ESD S20.20 and NFPA 99 requirements. After the conductive floor is cured, post-install electrical testing verifies continuity to ground at each grounding point.
Yes. PumaCRETE offers three buying options: complete turnkey installation through our nationwide network of factory-trained certified applicators (including EP Floors Corp. as our New England installer partner), materials-only supply with detailed installation instructions, videos, specialty tools, and surface prep guidelines for your own crew or contractor, or on-site factory training to qualify your own installers on conductive systems.
PumaCRETE offers conductive systems with conductivity as low as 400,000 ohms — and our specialty -c (conductive) systems achieve below 300,000 ohms. The standard ANSI/ESD definition of a conductive floor is 25,000 ohms to 1.0 million ohms resistance to ground. By engineering below 300,000 ohms, PumaCRETE leaves headroom for the floor + footwear + body resistance test required by DoD 4145.26-m.
Yes. Every PumaCRETE conductive flooring turnkey installation includes post-install electrical testing to ESD S20.20, NFPA 99, or DoD 4145.26 — whichever standard governs the facility. Written compliance documentation is delivered for audit records. Test points are recorded across the installed area and at every grounding tape connection.
Related PumaCRETE Systems
Explore More Industrial Flooring
External Authority References
- DoD ASSIST Quick Search(opens in new tab) — official source for DoD Manual 4145.26-m and MIL-STD-1686C
- National Fire Protection Association (NFPA)(opens in new tab) — NFPA 99 for healthcare and flammable areas
- EOS/ESD Association(opens in new tab) — governs ANSI/ESD S20.20 and STM7/97 test methods
- ANSI Webstore(opens in new tab) — official source for ANSI/ESD S20.20 publication
EXPERIENCE AND EXPERTISE
THE PumaCRETE Difference
We have over 30 years of experience behind us. Customers can rest assure that the system we recommend shall be the most cost effective. We provide customized solutions for challenging issues.