Server Halls · NOC · UPS · Telecom · Colocation
Data Center Anti-Static Epoxy Floors
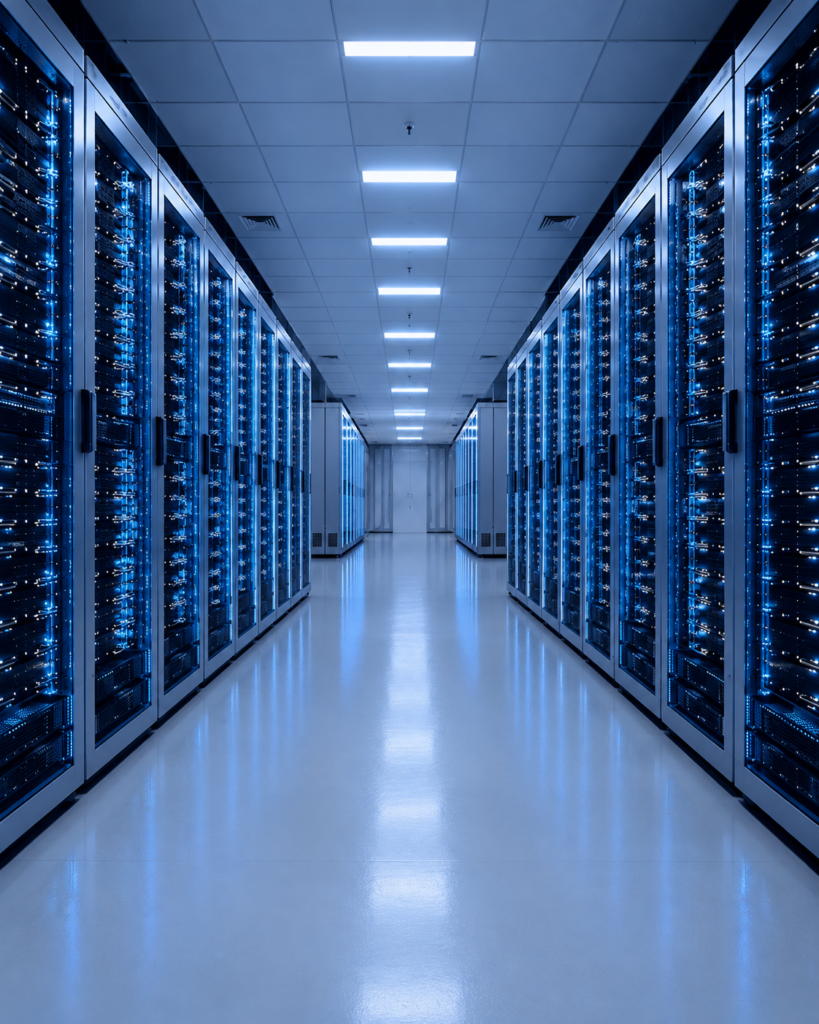
PumaCRETE® anti-static epoxy flooring engineered for data centers, server halls, NOC facilities, UPS rooms, and telecom infrastructure. ANSI/ESD S20.20 compliant. Body voltage below 15 volts. Moisture vapor handling up to 25 pounds per 1,000 sq ft per 24 hours — far exceeding the 3-pound limit of standard epoxy systems. Low-odor formulation allows installation in operating data centers without disrupting adjacent racks.
GET A FREE QUOTE

The PumaCRETE Buying Experience
Three Ways to Buy. One Engineered Anti-Static System.
PumaCRETE customizes the buying experience to match how your data center project is structured. Choose complete turnkey installation through our nationwide network of certified applicators, purchase materials only if you have your own crew or contractor (with detailed instructions, specialty tools, and surface prep guidelines included), or schedule expert on-site factory training to qualify your facilities team. One manufacturer, three ways to buy.
Why Data Centers Are Different
Data center flooring has different priorities than electronics manufacturing or munitions handling. Server halls and NOC facilities run 24/7 with strict uptime targets, racks cannot be shut down for major construction, and a single static discharge can corrupt data or silently flip bits in memory. The floor must control static, hold up under cart and pallet traffic delivering new equipment, withstand chemical spills from UPS battery rooms, and — critically — handle concrete moisture without delaminating. Most data center floor failures are not wear failures. They are moisture failures.
PumaCRETE engineers data center flooring around real operating conditions, not catalog ideals. The 104-PumaPOXY MB moisture blocker prime coat handles concrete vapor emissions up to 25 pounds per 1,000 square feet per 24-hour period — well beneith the failure point that defeats standard epoxy systems with their typical 3-pound limit. The anti-static urethane top coat dissipates static buildup from foot traffic and equipment carts, keeping body voltage below 15 volts per ANSI/ESD S20.20. And every material in the system is low odor, enabling installation work to proceed in occupied data centers without disrupting adjacent racks.
PumaCRETE customer base includes IBM, Lockheed Martin, Anduril Industries, NASA, and U.S. military facilities — operators who demand both ESD compliance and uptime preservation. Reference ANSI/ESD S20.20(opens in new tab) from the EOS/ESD Association for the static control standard.
Data Center Application Areas
Where PumaCRETE Anti-Static Flooring Is Specified
PumaCRETE anti-static flooring is installed across the full data center facility — wherever IT infrastructure, telecom equipment, or sensitive electronic hardware needs both static control and operational uptime.
Server Halls & White Space
Primary data hall floors, rack rows, hot/cold aisles. Often beneath raised access floor panels — PumaCRETE on the structural slab.
NOC Facilities
Network Operations Center workstations, monitoring walls, dispatch positions. Direct-applied anti-static finish, no raised floor needed.
UPS & Battery Rooms
Uninterruptible Power Supply rooms, VRLA and Li-ion battery storage. Chemical-resistant anti-static surface for spill containment.
Network Switching Rooms
Main Distribution Frames (MDF), Intermediate Distribution Frames (IDF), telecom cross-connects, fiber distribution.
Telecom Facilities
Carrier hotels, central offices, mobile switching centers, edge POP sites. Critical infrastructure with strict uptime requirements.
Colocation Suites
Multi-tenant data center suites, cage-and-cabinet colocation, hyperscale wholesale floors. Consistent ESD surface across the facility.
Equipment Staging
Receiving, unboxing, kit-testing, and burn-in zones where new equipment arrives before deployment to production racks.
DR & Backup Sites
Disaster recovery facilities, backup data centers, secondary network sites. Same ESD protection requirements as primary sites.
DR & Backup Sites
Disaster recovery facilities, backup data centers, secondary network sites. Same ESD protection requirements as primary sites.
Four Common Floor Problems
Why AGV and AMR Fleets Stop Working
Most AGV and AMR performance failures trace back to four classic floor problems. PumaCRETE 201-AGV and 301-AGV systems are engineered to fix all four.
117-PumaCOVE Resin Patching
High-strength epoxy patching material pre-fills holes, cracks, and major damage. Restores substrate to flat, sound surface before topcoat application.
104-PumaPOXY MB Primer
Moisture-blocking prime coat. Handles concrete vapor up to 25 lb / 1,000 sq ft / 24 hr. Applied over new concrete after 7-10 days cure. The single biggest differentiator vs standard data center epoxy.
104-PumaPOXY MB Mid Coat
Optional additional moisture-blocking coat. Recommended for renovation projects, high-moisture substrate conditions, or where extra protection is specified.
Anti-Static Urethane Top Coat
Anti-static urethane finish. ANSI/ESD S20.20 compliant. Body voltage below 15 volts. Seamless, low-odor, abrasion-resistant. Matte or low-sheen finish.
ESD Epoxy Flooring System Types
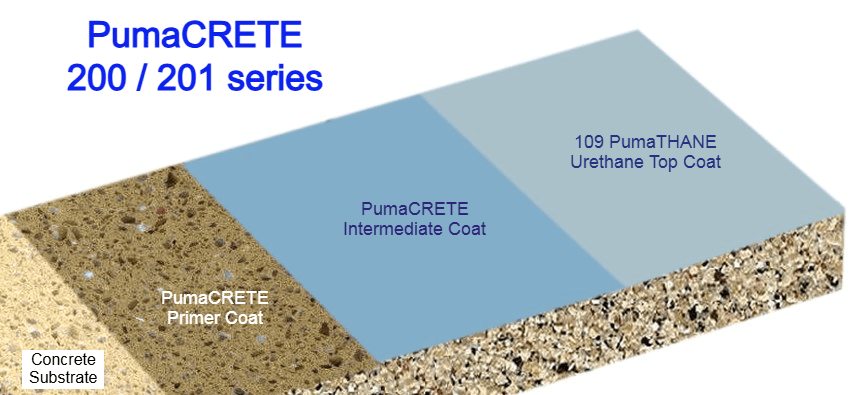
Thin Film Conductive Coatings
Best for light-duty to medium duty environments and controlled spaces.
FEATURES
- Meet ESD S20.20, DoD4145.26m, NFPA99 requirements.
- Smooth finish (or light texture)
- High abrasion resistance for heavy foot traffic, carts and wheeled loads.
- Easy to clean
- Chemical resistan
Heavy-Duty Conductive Mortar Systems 1/16 to 1/4 inch
Used in the most demanding environments.
FEATURES
- Restores damaged concrete
- Impact resistance
- High compressive strength
- Extended lifecycle performance
- Meets ESD S20.20, DoD4145.26m, NFPA99 requirements.
- Chemical resistant
Best for medium to heavy duty environments.
- Smooth finish (or light texture)
- High abrasion resistance for heavy traffic including forklifts, rubber and plastic wheels.
- Easy to clean
Technical Specifications
Standards-Backed Data Center Performance
PumaCRETE data center systems meet every threshold in ANSI/ESD S20.20(opens in new tab). Moisture vapor handling tested per ASTM F1869 (calcium chloride) and ASTM F2170 (relative humidity in-situ probe). Compliance context in Construction Specifier(opens in new tab).
| Specification | Data Center Requirement | PumaCRETE Achievement |
|---|---|---|
| Surface resistance (STM7.1) | Below 1.0×10&sup9; ohms | 1×10&sup6; – 1×10&sup9; ohms |
| Body voltage (STM97.2) | Below 100 volts | Below 15 volts |
| Moisture vapor handling | Typical competitor limit: 3 lbs/1,000 sq ft/24 hr | Up to 25 lbs/1,000 sq ft/24 hr |
| VOC / odor | Important for 24/7 facilities | Low odor — minimal racks-adjacent impact |
| Surface finish | Seamless (no dust traps) | Monolithic, no seams or joints |
| Maintenance to preserve ESD | n/a | None — no wax, no recoating |
| Chemical resistance | Needed for UPS battery rooms | Resistant to battery electrolyte, oils |
| Service temperature | Cold aisle / hot aisle stable | -20°F to +200°F |
PumaCRETE Coating vs Raised Access Floor — Which Do You Need?
Raised access floor systems (Tate, ASM Modular) and PumaCRETE coating are often complementary, not competitive. Many data centers use both. Here’s how to decide.
| Factor | PumaCRETE Anti-Static Coating | Raised Access Floor (Tate, ASM) |
|---|---|---|
| Best for | NOC, UPS, telecom, MDF/IDF, server hall sub-floor | Server hall white space with under-floor cabling/cooling |
| Cable management | Overhead trays or wall raceways | Under-floor plenum |
| Air handling | Overhead supply, hot/cold containment | Under-floor cold supply via perforated tiles |
| Installation cost | Lower (no pedestals, no panels) | Higher (panels + structure) |
| Joint / seam risk | None — monolithic | Panel edges may wear, accumulate dust |
| Often combined? | Yes — PumaCRETE on slab beneath raised floor for moisture & dust control | Yes — same arrangement |
PumaCRETE vs Other Data Center Coating Manufacturers
Most data center coating manufacturers — Sherwin-Williams, Stonhard, Sika, Tnemec, Florock — meet ANSI/ESD S20.20. The differences are in moisture vapor handling, buying flexibility, and the system layer depth.
| Capability | PumaCRETE 200 Series | Typical Competitor Range |
|---|---|---|
| Moisture vapor handling | Up to 25 lb / 1,000 sq ft / 24 hr | 3 lb / 1,000 sq ft / 24 hr typical |
| Body voltage achieved | Below 15V | 25–80V typical |
| Buying options | Turnkey · materials · training | Typically turnkey only |
| Low-odor for occupied install | Yes — minimal racks-adjacent impact | Varies; some require shutdown |
| Conductive element location | Graphite throughout matrix | Often topical or single layer |
| Post-install testing | Included with turnkey | Often extra-cost service |
Comparison based on publicly published competitor data. PumaCRETE is not affiliated with Sherwin-Williams, Stonhard, Sika, Tnemec, Florock, Tate Access Floors, ASM Modular Systems, or StaticWorx. Trademarks belong to their respective owners.
Installation & Certification
Installed by Factory-Trained Certified Applicators
Every PumaCRETE turnkey data center installation is delivered by factory-trained, factory-certified applicators working from our nationwide installer network. In the New England region, our certified installer partner EP Floors Corp. (Three Rivers, MA) handles many data center installations including server rooms and NOC facilities. We do not sub-contract to unknown crews. Every installer has been trained at PumaCRETE on moisture testing, substrate prep, the 200 Series layer system, ESD resistance testing per ANSI/ESD S20.20, and phased installation procedures that maintain data center uptime — and every installation is backed by a manufacturer-plus-installer warranty.
Four-Step 200 Series Installation Process
1. Moisture Test + Surface Prep
On-site evaluation. ASTM F1869 calcium chloride and/or ASTM F2170 in-situ probe moisture testing. Concrete condition mapped — cracks, holes, spalls, joints. 117-PumaCOVE Resin epoxy patching of damage. Diamond grinding or shotblasting to CSP 3 profile.
2. 104-PumaPOXY MB Moisture Block
Moisture blocker primer applied. Coverage rate verified for the measured vapor emission rate. Optional mid coat for renovation or high-moisture substrate. Cure per spec.
3. Anti-Static Urethane Top Coat
Anti-static urethane finish applied. Color and matte finish per facility specification. Low-odor formulation enables work to proceed in zones adjacent to operating racks.
4. ESD Test & Acceptance
Post-install ESD resistance testing per ANSI/ESD S20.20 STM7.1, STM97.1, and STM97.2. Multi-point grid testing. Written compliance certification delivered for audit. Manufacturer + installer warranty active.
Phased Installation for 24/7 Data Centers
Data centers cannot shut down for major flooring work. PumaCRETE installations in operating facilities are phased: defined zones (1–4 rack rows at a time) are completed during planned maintenance windows or off-peak periods. Rack equipment is temporarily relocated within the white space, the floor is installed and cured, and equipment is restored before crews move to the next zone. Low-odor PumaCRETE materials enable adjacent zones to remain in service throughout.
Materials-Only & Factory Training
If your data center has an existing flooring contractor relationship, PumaCRETE ships 200 Series materials direct, with detailed installation instructions, moisture testing protocols, specialty tools, and surface prep guidelines. Or schedule on-site factory training to qualify your in-house facilities team for ongoing maintenance and future data center expansions.
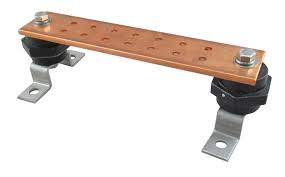
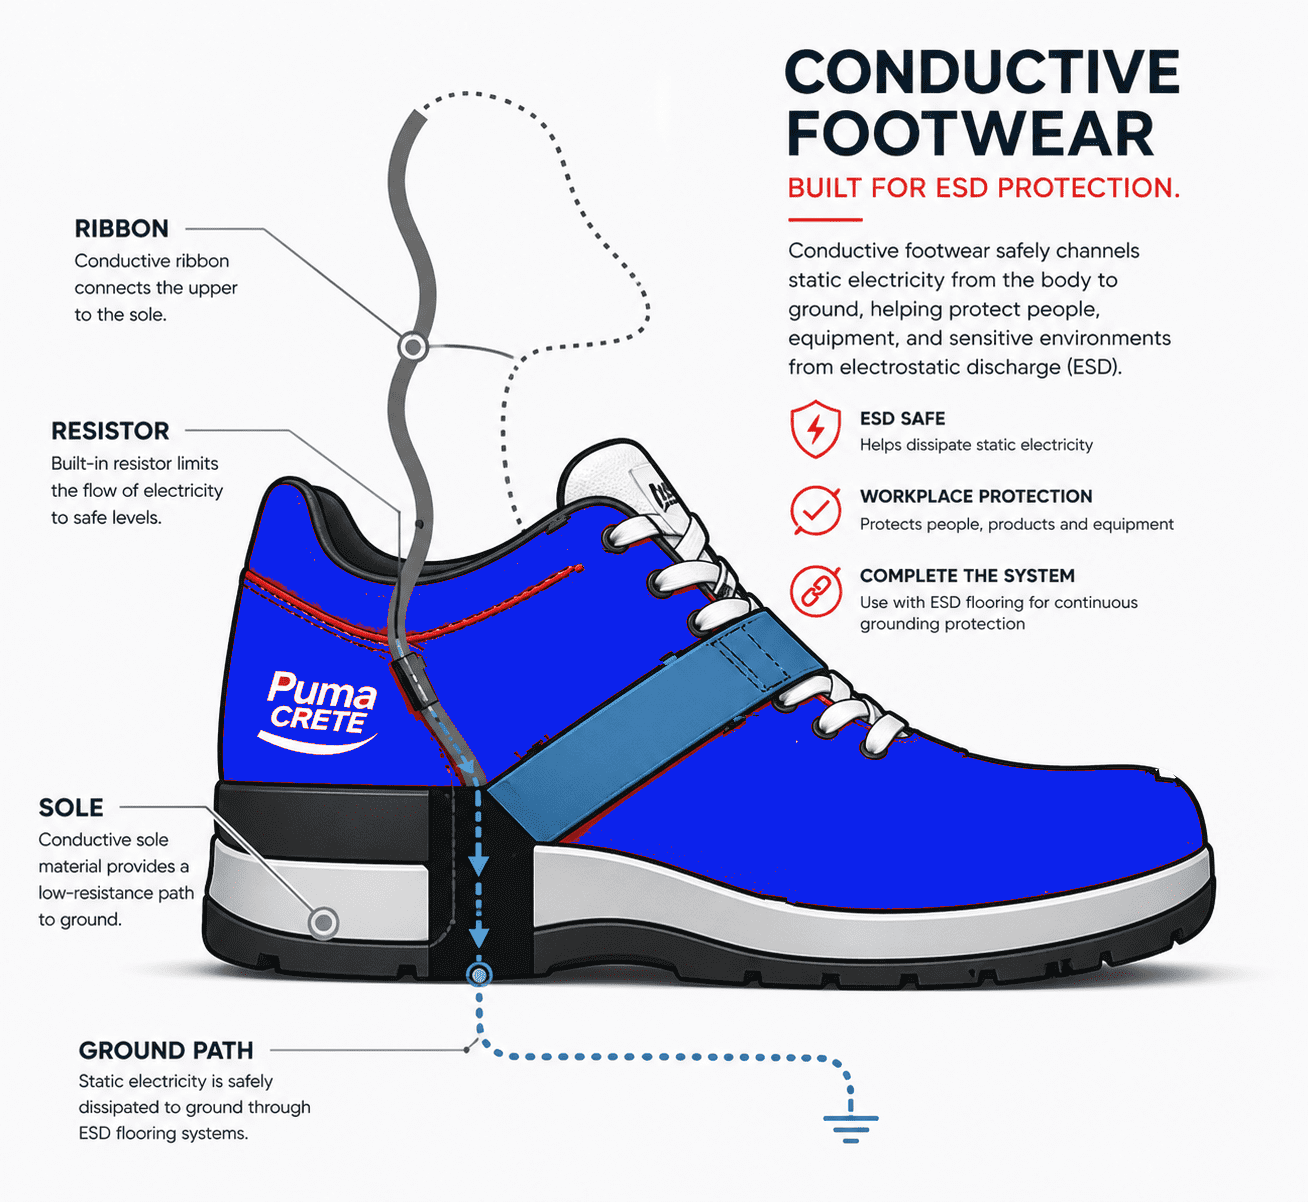
EARTH GROUND (copper ground rod, bar, outlet.
Copper ground rods are often used in Military, Munitions, and manufacturing environments. At the ground point on rod... remove oxidation from rod (for connection with a clamp). Run copper foil tape on the floor, per figure 2. Run the tape up the ground rod, and secure tape to ground rod using the copper foil tape.
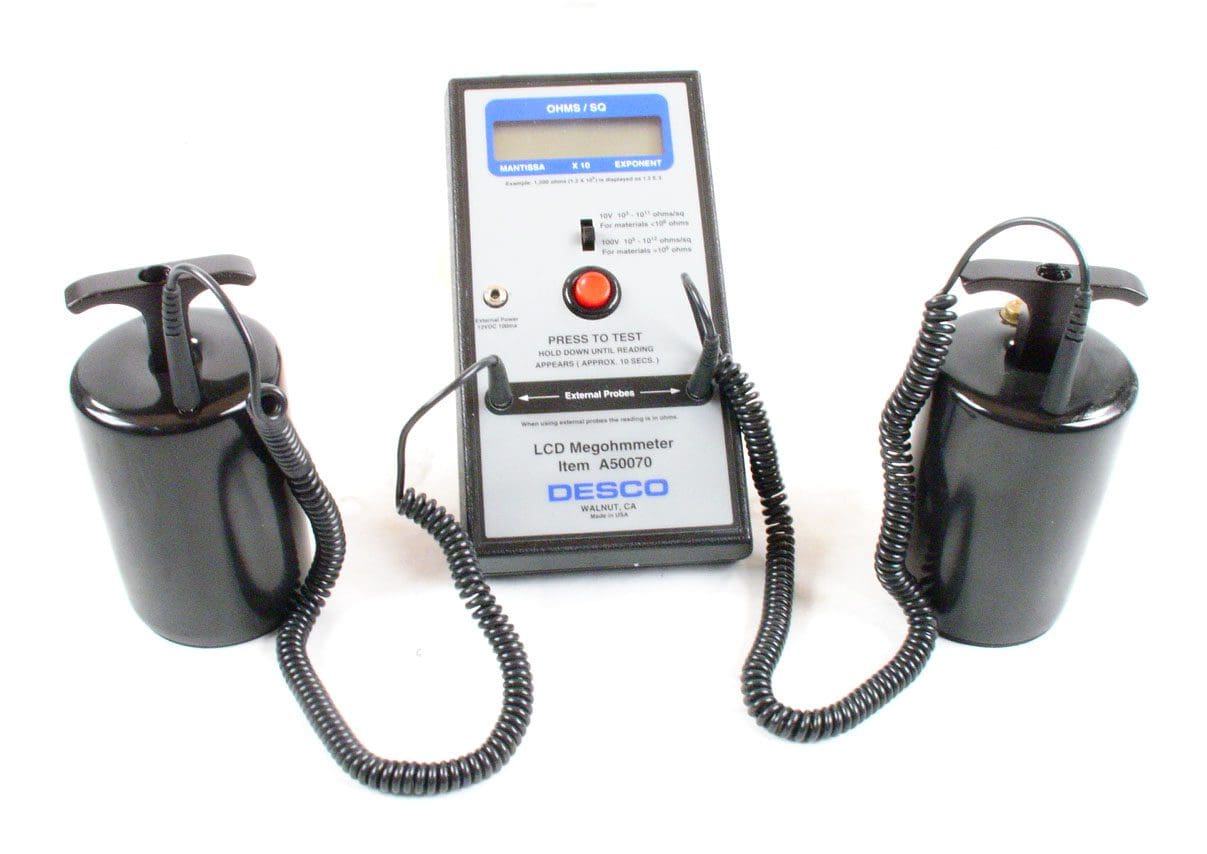
Certify the Flooring meets:
DoD 4145.26M(opens in new tab) ESD Association S20.20(opens in new tab) NFPA(opens in new tab) OSHA(opens in new tab)
Certify the Flooring meets:
DoD 4145.26M(opens in new tab) ESD Association S20.20(opens in new tab) NFPA(opens in new tab) OSHA
NATIONWIDE NETWORK OF INSTALLATION
With a nationwide network of installers, PumaCRETE® has provides a tradition of quality. Our factory-trained installation crews can provide turn-key installation and localized service. In many cases, we can train your personnel or local contractor, with on site training available.
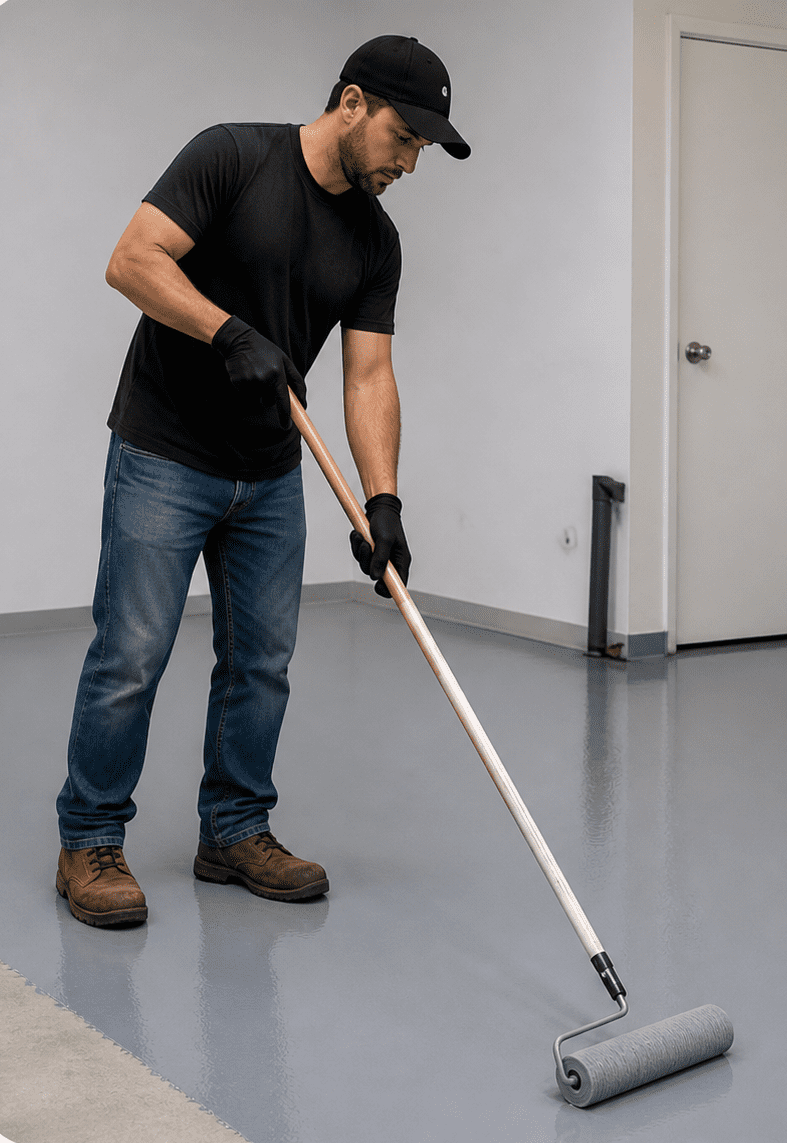
PumaCRETE® SITE TRAINERS
PumaCRETE® can provide on site trainers, along with detailed installation instructions and videos, specialty tools, and surface prep guidelines for new installers or DIY installation. See our installation page for our application resources.
Frequently Asked Questions
AGV / AMR Flooring FAQ
Server hardware, network switching equipment, storage arrays, and UPS systems are all ESD-sensitive — a single static discharge can corrupt data, trigger reboots, damage components, or cause silent bit-flips that take days to diagnose. Anti-static flooring continuously bleeds off static accumulation from personnel and equipment carts moving through the white space, keeping body voltage below the ESD damage threshold for server hardware. PumaCRETE meets ANSI/ESD S20.20 with body voltage below 15 volts.
Server halls and white space, NOC (Network Operations Center) facilities, network switching rooms, UPS rooms and battery rooms, telecom rooms and main distribution frames (MDF), intermediate distribution frames (IDF), colocation suites, equipment staging areas, and dedicated kit testing spaces. Anywhere personnel touch energized ESD-sensitive IT infrastructure.
PumaCRETE includes the 104-PumaPOXY MB moisture blocker prime coat that handles concrete vapor emissions up to 25 pounds per 1,000 square feet per 24-hour period — far exceeding the typical 3-pound limit of standard epoxy systems. This prevents delamination, blistering, and cracking caused by concrete moisture, which is the single most common cause of data center floor failures.
Yes. PumaCRETE materials are low odor, which minimizes interference with adjacent ongoing operations — important for 24/7 data centers where racks cannot be shut down during flooring work. Installation is typically phased: PumaCRETE crews work in defined zones during planned maintenance windows or off-peak hours, with rack equipment temporarily relocated and the floor restored before traffic returns to that zone.
Raised access floor systems (Tate, ASM Modular) are panels suspended on pedestals above the structural slab, creating an under-floor void for cable management and cold-air supply. PumaCRETE is a coating applied directly to the structural slab. The two are often complementary — many data centers use raised access floor panels in the white space AND PumaCRETE on the slab below the raised floor to control dust, moisture, and provide an ESD-grounded sub-floor. PumaCRETE is also used directly as the working floor in NOC rooms, UPS rooms, and telecom rooms where cable management is overhead or in cable trays rather than under the floor.
Yes. PumaCRETE offers three buying options for data center operators: complete turnkey installation through our nationwide certified installer partner network (including EP Floors Corp. as our New England partner), materials-only supply for existing flooring contractors with detailed installation instructions, specialty tools, and surface prep guidelines, or on-site factory training to qualify your in-house facilities team for ongoing maintenance and future expansions.
The 200 Series PumaCRETE is a roll-on coating system for new concrete and concrete in good condition. The full system includes: surface prep with 117-PumaCOVE Resin epoxy patching of cracks, holes, and damage; 104-PumaPOXY MB moisture blocker prime coat; optional 104-PumaPOXY MB mid coat for renovation projects with elevated moisture or for additional protection; and an anti-static urethane top coat. The result is a seamless, monolithic, anti-static surface with full ANSI/ESD S20.20 compliance.
Related PumaCRETE Systems
Explore More Industrial Flooring
External Authority References
International Electrotechnical Commission (IEC)(opens in new tab) — governs DIN EN 61340-5-1 ESD floor standard
EOS/ESD Association(opens in new tab) — ANSI/ESD S20.20 + STM7/97 test methods
Material Handling Industry of America (MHI)(opens in new tab) — AGV/AMR industry body and ProMat reference
Construction Specifier(opens in new tab) — flooring spec resource for AGV/AMR areas
EXPERIENCE AND EXPERTISE
THE PumaCRETE Difference
We have over 30 years of experience behind us. Customers can rest assure that the system we recommend shall be the most cost effective. We provide customized solutions for challenging issues.